CNC Machining for the Automotive Industry
22 min
- What Is Automotive CNC Machining?
- What Automotive Parts Can Be CNC Machined?
- When Is CNC Machining the Right Choice for Automotive Parts?
- What CNC Machining Processes Are Used for Automotive Parts?
- What Materials Are Used for CNC Machined Automotive Parts?
- What Tolerances and Surface Finishes Do Automotive CNC Parts Require?
- What Affects the Cost of Automotive CNC Machining?
- How to Choose an Automotive CNC Machining Supplier?
- Automotive CNC Machining FAQs
- Conclusion About Automotive CNC Machining
Key Takeaways
- Automotive CNC machining is used both to produce certain low-volume components directly and to finish cast or forged parts at critical interfaces, including engine blocks, transmission housings, suspension uprights, brake components, and EV motor housings.
- CNC machining isn't how most automotive parts get manufactured in volume; casting, forging, and stamping handle the majority of mass production.
- What CNC does well is prototyping, low-volume production, precision finishing of cast or forged parts, and the machining of critical interfaces on increasingly complex EV components.
- Automotive CNC tolerances are defined by the function of each feature rather than by a single industry-wide value. General dimensions may use relatively loose tolerances, while fit-critical features can require tighter dimensional and geometric controls, specialized finishing, and dedicated inspection.
- Material choice is driven by the mechanical and thermal demands of the specific component.
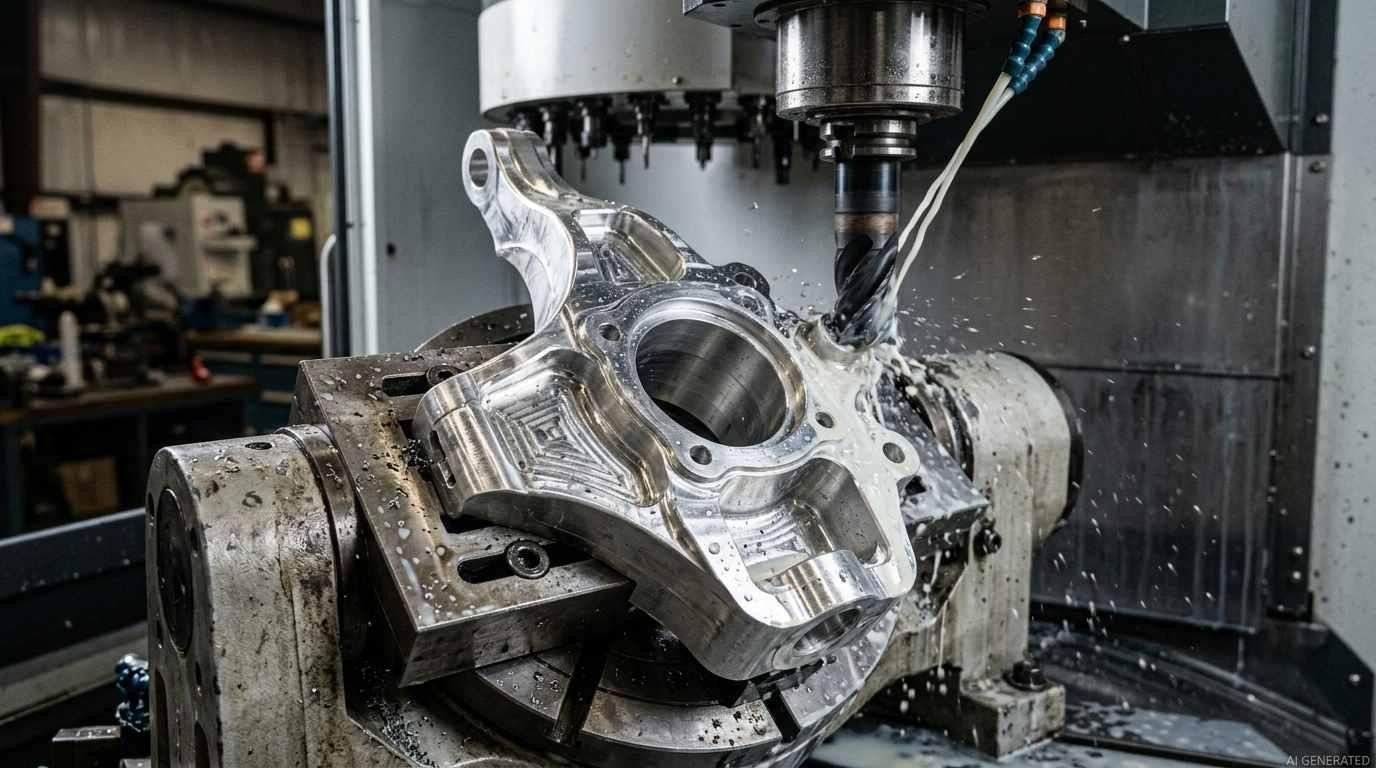
Machining a precision automotive component
In automotive manufacturing, "machined" can describe either a part produced largely by CNC or a cast or forged blank that receives CNC finishing at function-critical interfaces. An engine block may be cast and then machined at cylinder bores, bearing bores, deck surfaces, and threaded holes, while a suspension upright may be machined from billet for a prototype or low-volume application.
Understanding where CNC machining actually fits in automotive manufacturing, what it does well, and where other processes make more sense is the practical foundation this guide is built on.
What Is Automotive CNC Machining?
Automotive CNC machining uses computer-controlled milling, turning, and multi-axis machining centers to produce components from metal or plastic stock or to finish critical features on cast and forged blanks. The machine follows programmed tool paths derived from CAD geometry, producing parts with controlled dimensions, tolerances, and surface finishes.
For a deeper look at how CNC machining works, from CAD and toolpaths to the finished part, see our guide to CNC parts and how they are made.
What Automotive Parts Can Be CNC Machined?
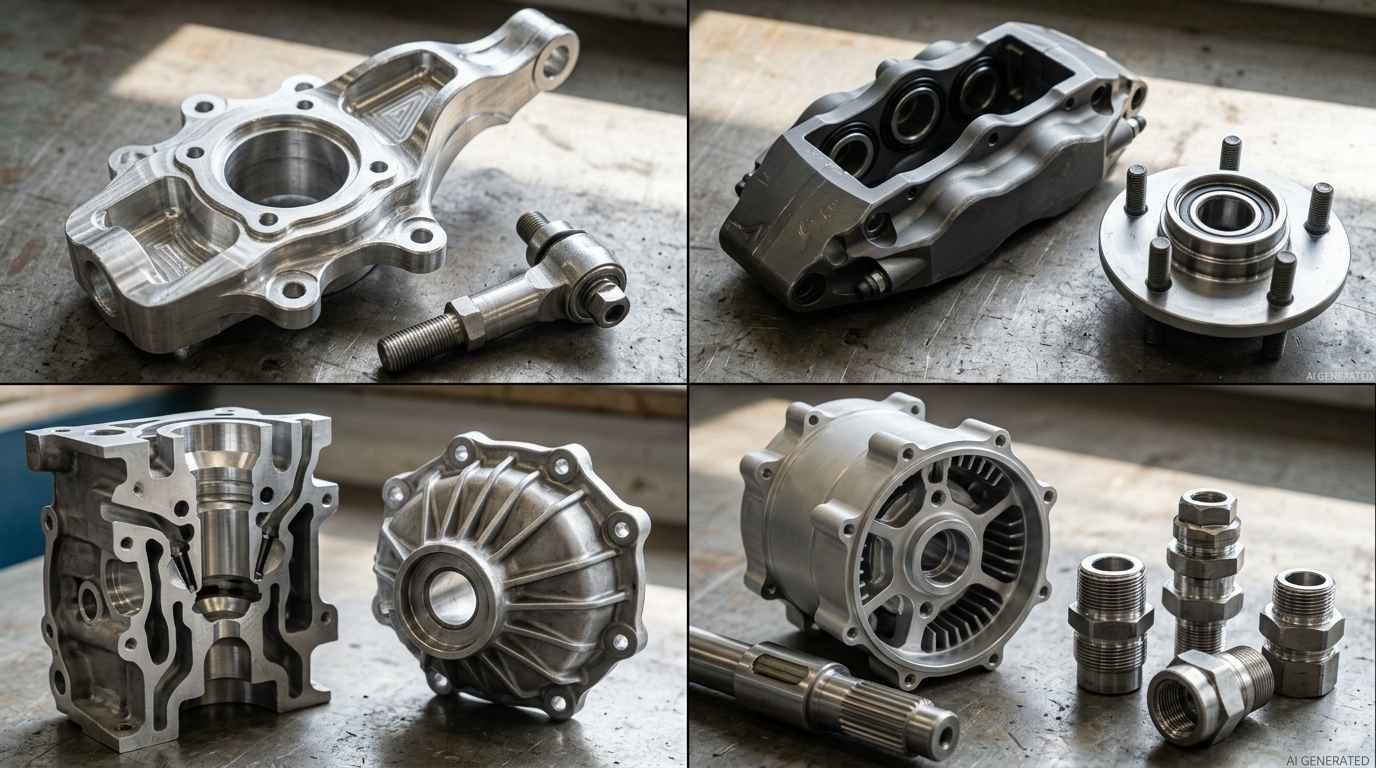
Collection of CNC machined automotive components
Engine and Powertrain Components
Engine components represent some of the most demanding automotive machining work. Cylinder blocks and heads are typically cast. The complex internal geometry of cooling passages and combustion chambers is difficult or impossible to machine from solid. But the precision features on those castings are machined: bore surfaces, valve seat inserts, cam bearing bores, oil passages, and mating faces all need tolerances and surface finishes that the casting process can't achieve directly.
Crankshafts are commonly forged and then machined through multiple operations, with bearing journals typically finished by turning, grinding, or other dedicated processes to achieve the required diameter, roundness, and surface condition. Connecting rods are machined from forged blanks. Intake manifolds are sometimes machined from billet aluminum for performance applications where the casting tooling cost isn't justified. Transmission housings, selector forks, differential components, shafts, and other powertrain parts may require substantial CNC machining at bearing seats, mounting interfaces, bores, threads, and other precision features.
Chassis, Suspension, and Steering Components
Suspension geometry determines how a vehicle handles, and the parts that define that geometry need to hold their dimensions under significant dynamic loads. Suspension uprights (knuckles), control arm mounting brackets, tie rod ends, and steering rack housings are all candidates for CNC machining. In volume passenger car production these might be cast or forged with machined finish operations. In motorsport and aftermarket applications, billet machined uprights and control arms are common because the quantities don't justify tooling and the geometry can be optimized more readily without mold constraints.
Wheel hubs and bearing housings need precise bore dimensions for bearing fits. Subframe mounts, chassis brackets, and crossmember components often combine stamped steel structure with machined interfaces at critical connection points.
Braking, Fluid, and Thermal Components
Brake calipers are one of the most commonly cited examples of precision automotive CNC machining. A caliper needs accurate piston bore geometry, precise port positioning, clean thread forms for bleeder screws and brake line fittings, and smooth sealing surfaces. High-performance aftermarket calipers are often machined from billet aluminum entirely. OEM calipers are typically cast with precision-machined bores and faces.
Brake master cylinders and ABS modulator valve bodies are machined from aluminum or steel with tight bore tolerances. Hydraulic fittings and adapters, coolant manifolds, heat exchangers, oil coolers, and their mounting components all involve CNC machined parts at various levels of complexity.
Electrical and Sensor Components
Automotive sensors are increasingly sophisticated, and their housings and mounting brackets often require precision machined geometry. CNC machining is commonly used for sensor mounting features, housings, bores, and other interfaces where feature location affects sensing performance. In reluctor and target-wheel assemblies, radial or axial position, runout, and mounting repeatability can matter as much as nominal dimensions.
Electrical connector housings, ECU mounting plates, and ground bus bars in high-voltage systems all show up as machined components, especially in low-volume or prototype programs where injection molding tooling isn't justified.
EV Battery, Motor, and Power Electronics Components
Electric vehicle development has significantly expanded the role of CNC machining in automotive manufacturing. EV programs have expanded the range of components that require CNC-machined interfaces. Battery trays and enclosures may combine extrusion, sheet or casting processes with CNC machining for sealing surfaces, mounting faces, holes, and locating features. Motor housings are also commonly cast and then CNC machined at bearing bores, end faces, mounting features, and other alignment-critical surfaces.
Motor housings for permanent magnet motors need precise bore geometry for stator press fits, precisely located bearing bores for rotor alignment, and often complex cooling jacket geometries with internal channels. Battery pack structures combine machined aluminum housings with precise cell mounting features. Power electronics housings need controlled thermal interface surfaces and precise connector locations. As EV volumes increase, production routes often shift toward casting, extrusion, or other near-net-shape processes for larger structures, while CNC remains important for finishing the interfaces that control assembly, sealing, alignment, and thermal performance.
For a closer look at how CNC machining is used for EV battery boxes, motor housings, cooling components, and other NEV parts, see our guide to EV battery and motor housing machining.
Precision CNC Machining Service
Have an automotive part ready for machining? Upload your CAD file for engineering review and a quote. JLCCNC can review the geometry, material, tolerances, and production requirements before machining.
When Is CNC Machining the Right Choice for Automotive Parts?
| Factor | CNC Machining | Casting | Forging | Stamping |
|---|---|---|---|---|
| Dedicated tooling | Low | High | High | High |
| Best fit by volume | Prototype to low/mid volume | Medium to high volume | Medium to high volume | High-volume sheet parts |
| Geometry | High flexibility but limited by tool access | Complex external and internal geometry | Strong bulk geometry with material-flow benefits | Sheet-based geometry |
| Critical features | Machined directly | Often require secondary machining | Often require secondary machining | Secondary machining may be needed |
| Design changes | Fast | Slow after tooling | Slow after tooling | Slow after tooling |
| Typical automotive use | Prototypes, low-volume parts, precision interfaces | Blocks, housings, complex cast structures | Shafts, rods, structural/load-bearing components | Body and sheet-metal structures |
Automotive Prototyping and Design Validation
CNC machining is particularly useful during automotive development when engineers need a functional prototype with the intended material and final geometry before committing to production tooling. Typical prototype applications include revised suspension geometry for vehicle testing, intake manifolds for dyno validation, and EV battery housings used for interference and assembly checks before production tooling is released.
A machined aluminum brake caliper prototype has the thermal properties and structural behavior of aluminum. That's not true of 3D printed prototypes in most materials, which is why CNC machining remains important even as additive manufacturing has expanded in automotive R&D.
Low-Volume and Specialty Production
Racing series, limited-edition vehicles, classic car restoration, and specialized commercial vehicles all generate demand for parts in quantities that don't justify casting or forging tooling.
For example, a short run of billet differential covers, suspension brackets, or prototype housings may be machined directly from stock when dedicated casting or forging tooling would not be justified.
Motorsport, Aftermarket, and Service Parts
Motorsport has driven automotive CNC machining capability for decades. Motorsport programs often use CNC machining for low-volume components whose geometry changes frequently or benefits from billet stock, but any material substitution still has to be validated against strength, fatigue, wear, thermal loads, and the intended load path.
The aftermarket parts market follows similar logic. Upgraded brake calipers, billet throttle bodies, performance intake manifolds, and replacement components are common candidates for CNC machining when volumes are too small to justify dedicated casting or forming tooling. Replacement parts may be machined from current drawings or validated reverse-engineered data when the original tooling is unavailable. Using a worn component as the sole dimensional reference can reproduce wear rather than the intended geometry, so critical features should be verified against design requirements before machining.
Secondary Machining of Cast or Forged Parts
Many automotive parts enter CNC machining as cast or forged blanks rather than solid stock. CNC operations then establish features that control assembly, sealing, alignment, or bearing fit, such as bores, mounting faces, threaded ports, and other precision interfaces.
An engine block casting, for example, may require machining of cylinder bores, main-bearing bores, deck surfaces, threaded holes, and other assembly interfaces after casting. The cast block provides the complex internal geometry of water jackets and oil passages. The machining provides the dimensional precision that enables bearing fits, head sealing, and proper piston-to-bore clearances.
What CNC Machining Processes Are Used for Automotive Parts?
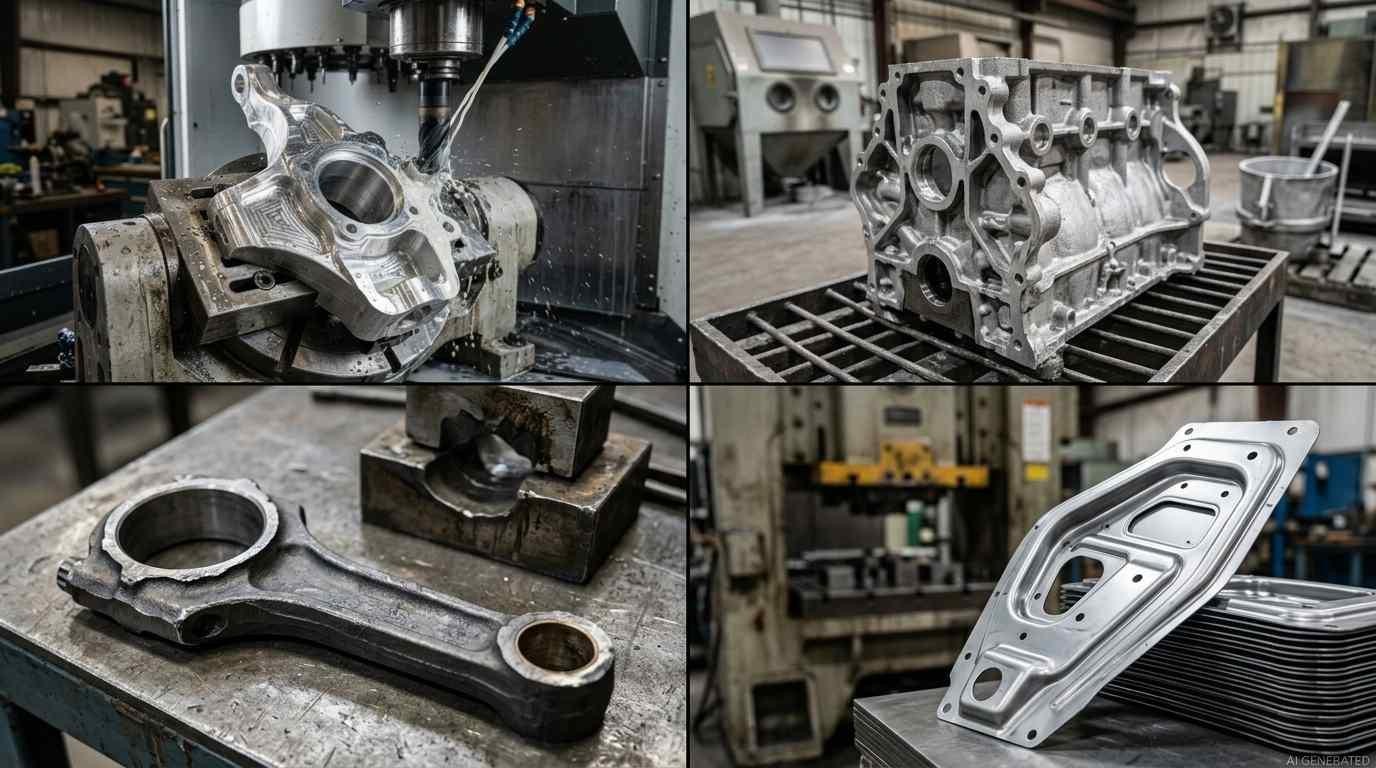
automotive manufacturing comparison
CNC Milling
Milling is the most common process for automotive CNC machining of prismatic parts, blocks, housings, brackets, flanges, and plates. Multi-axis milling machines move a rotating cutter through controlled paths to produce flat surfaces, pockets, slots, complex contours, and drilled features.
3-axis milling covers the majority of automotive component machining where features are accessible from standard orientations. 5-axis machining becomes valuable when critical features are distributed across multiple faces, when tool access is restricted by deep or angled geometry, or when fewer setups can improve the relationship between features referenced to common datums. Automotive examples include complex housings, angled ports, multi-face mounting features, and components with difficult tool access.
CNC Turning
Turning produces cylindrical geometry: shafts, spindles, pistons, crankshaft journals, bearing races, hubs. The workpiece rotates while a cutting tool follows a programmed path. Modern CNC turning centers may use live tooling, allowing cross-drilled holes, flats, keyways, and other milling features to be produced without moving the part to a separate machine.
Automotive crankshafts, camshafts, driveshafts, axles, and wheel spindles all involve significant turning operations. Piston OD, pin bore, and ring groove geometries are turned to tight tolerances that affect engine compression and oil consumption.
Drilling, Boring, and Threading
Automotive components have extensive hole features, oil passages, coolant ports, fastener holes, sensor mounting threads, hydraulic ports. Drilling produces the initial geometry. Boring (single-point cutting of an existing hole) achieves the precision diameter and roundness needed for bearing fits and sealing applications. Threading, by tapping or thread milling, creates the fastener interfaces that hold powertrains, suspension, and chassis components together.
Thread quality in automotive machining matters more than it sounds. A spark plug thread that's torn rather than cut will strip under thermal cycling. A caliper bleeder screw thread that's poorly formed leaks. Getting threading right is part of the manufacturing quality picture.
4-Axis and 5-Axis CNC Machining
4-axis machining adds rotary motion around one of the linear axes, allowing a part to be indexed or continuously rotated so features on multiple sides can be machined without fully reorienting the workpiece. Useful for shaft components that need machined features around their circumference, keyways, cross-drilled holes, flats on a shaft.
5-axis machining becomes valuable when critical features are distributed across multiple faces, when tool access is restricted by deep or angled geometry, or when reducing re-fixturing can improve feature-to-feature accuracy. It is not automatically the lowest-cost option; for simpler parts, 3-axis machining or 3+2 positioning may achieve the same functional result with less machine time and setup complexity.
What Materials Are Used for CNC Machined Automotive Parts?
Aluminum
Aluminum dominates modern automotive CNC machining for weight-sensitive applications. 6061-T6 is the workhorse, good machinability, adequate strength for most brackets and housings, excellent corrosion resistance, and compatible with anodizing. 7075-T6 is selected when higher strength-to-weight performance is needed, particularly for certain high-stress brackets, housings, spacers, and aftermarket or motorsport components. Cast aluminum alloys (A356, A380) are common in cast-then-machined components like engine blocks and transmission cases.
EV motor housings and battery enclosures have driven significant growth in aluminum CNC machining in automotive manufacturing, as these components need complex geometry, good thermal conductivity, and adequate structural performance at manageable weight.
Steel and Stainless Steel
Steel goes where aluminum doesn't have enough strength or wear resistance. Crankshafts, camshafts, gears, drive shafts, and structural fasteners are typically steel, either alloy steels like 4140 and 4340 that machine well and respond to heat treatment, or higher-alloy grades for specific applications.
Stainless steel grades vary by application. Grade 409 is widely used in automotive exhaust systems because it combines adequate high-temperature corrosion resistance with lower alloy cost, while 304 is used where higher corrosion resistance or appearance requirements justify the added cost. Grade 316 is more specialized and is generally selected when its higher corrosion resistance is actually needed.
Brass and Copper
Brass is commonly used for fittings, connectors, adapters, and other small components where machinability and corrosion resistance are important. Copper is more relevant to bus bars and thermal-management components because of its high electrical and thermal conductivity. Its combination of machinability, corrosion resistance, and appropriate hardness for threaded hydraulic connections makes it well-suited for small precision fittings.
Copper appears in EV thermal management, heat exchanger components, busbar connections, and thermal interface plates where high electrical and thermal conductivity are primary requirements.
EV architectures introduce more copper-intensive electrical and thermal components, increasing the number of applications where machined copper or copper-alloy features may be required.
Engineering Plastics
Machined plastics in automotive applications cover a specific niche: electrical insulators, bearing bushings, seal housings, and prototype interior components. Delrin (acetal/POM) is common for sliding contact components, small precision fittings, and gear components where its low friction and dimensional stability suit the application. PEEK appears in high-temperature under-hood applications where most plastics would fail. Nylon grades handle moderate structural loads with good chemical resistance in fluid contact applications.
What Tolerances and Surface Finishes Do Automotive CNC Parts Require?
Dimensional and Geometric Tolerances
Automotive tolerances span a wide range depending on what the part does. Automotive drawings do not use a single CNC tolerance. General dimensions may follow a specified general-tolerance standard, while fit-critical features are controlled by individual size limits, fit classes, and geometric tolerances.
Bearing seats, for example, should be specified according to the required shaft or housing fit and nominal diameter rather than a blanket ± tolerance. ISO 286 provides standardized tolerance classes for holes and shafts, while additional form and surface requirements may be needed to control the actual fit.
Cylinder bores are controlled by more than diameter alone. Depending on the engine design, the drawing or process specification may control bore size, roundness, cylindricity, taper, piston-to-bore clearance, and the final honing texture.
Automotive drawings commonly use GD&T controls such as position, perpendicularity, flatness, profile, and runout to control the relationships between mounting surfaces, bores, holes, and rotating features. A brake caliper bore that's dimensionally correct but not perpendicular to the mounting face will cause the pads to contact unevenly. A crankshaft journal that's round but not concentric to the main bearing axis causes vibration.
Surface Finish Requirements
Surface finish requirements depend on the type of interface and operating condition. For example, Parker specifies Ra up to 1.6 µm for non-pulsating static O-ring contact surfaces, 0.8 µm for pulsating static applications, and 0.4 µm for dynamic sealing surfaces; groove surfaces can permit higher roughness depending on the sealing arrangement.
Bearing-related surfaces also vary with their function. For bearing seats, SKF specifies Ra below 3.2 µm for some h7 shaft-seat applications and below 1.6 µm for h6 applications, while its seal guidance recommends roughly Ra 0.2–0.6 µm for standard shaft sealing surfaces and 0.2–0.4 µm at higher speeds.
These values are application references rather than a universal automotive specification. The drawing should define the required roughness together with the fit, sealing design, dimensional and geometric tolerances, material, and operating conditions. A tighter Ra requirement than the function requires can add grinding, honing, polishing, or additional inspection without improving the part.
Non-functional surfaces, such as the exterior of a bracket or the back face of a housing, typically require only an as-machined finish appropriate to the coating, assembly, or appearance requirement. Specifying surface finish tighter than the function requires adds machining time and cost for no benefit.
Choosing Tolerances Based on Part Function
The correct approach to tolerance specification is working backward from the functional requirement. What fit does this bore need to achieve? What clearance does this shaft require? What geometric relationship between these two features determines whether the assembly works correctly? The answers drive the tolerances, which then determine the machining approach and inspection method.
Over-specifying tolerances is a common and expensive mistake in automotive component design. A tight tolerance on a non-functional feature doesn't improve the part, it increases machining time, adds inspection burden, and raises rejection rates without improving how the assembly performs.
What Affects the Cost of Automotive CNC Machining?
Material, Size, Geometry, and Setup Complexity
Material is the starting point. In many CNC applications, aluminum alloys machine faster than common alloy steels, while titanium and nickel-based alloys generally require more conservative cutting conditions and closer tool-wear control. Raw material cost also varies significantly by grade and supply condition. Part size affects raw material cost and machine time directly. More complex geometry means more tool paths, more tool changes, and potentially more setups, each adding cost.
Setup count can be a larger cost driver than machine hourly rate. A higher-rate 5-axis machine can reduce total cost when it eliminates multiple setups, custom fixturing, or repeated datum recovery, while a simpler 3-axis process may remain more economical when all critical features are accessible with few setups.
Tolerances, Finishing, Inspection, and Documentation
Tighter tolerances increase machining time through additional finishing passes, in-process gauging, and higher rejection rates. Surface finishes beyond as-machined, anodizing, plating, powder coating, shot peening, add process steps and cost. Inspection frequency and documentation should be defined by the drawing, customer requirements, control plan, production risk, and the characteristics being verified. CMM inspection may be used for first-article approval, critical GD&T, or complex feature relationships, while production parts may use gauges, dedicated fixtures, or statistical sampling where those methods adequately verify the requirement.
In automotive supplier relationships, particularly for OEM supply, documentation requirements can be significant. PPAP (Production Part Approval Process) documentation, material certifications, and measurement reports add administrative cost that needs to be priced into the program.
For more on how CMM inspection verifies dimensions, geometric tolerances, and complex CNC features, see our CMM inspection guide.
Production Volume, Cycle Time, and Secondary Operations
Unit cost drops with quantity because setup costs amortize across more parts, tooling gets amortized, and production efficiency improves as the process is refined. A single prototype part carries the full weight of programming and setup time in its price. As quantity increases, programming, fixture, and initial setup costs are distributed across more parts, reducing their contribution to unit cost.
Surface treatments, heat treatment, grinding, honing, plating, and assembly all add process steps and cost. Heat treating steel components to required hardness adds cost and lead time. Post-machine honing of cylinder bores adds precision that turning and boring can't achieve but adds a process step. These secondary operations are necessary for the part to function correctly and can't be value-engineered out, but they need to be identified and priced from the start.
How to Choose an Automotive CNC Machining Supplier?
Machining Capability and Production Range
The first supplier-screening question is whether the shop has the machine capacity, process capability, and inspection resources required for the part. That means machine capability, appropriate axis count for the geometry, spindle power and rigidity for the materials involved, work envelope for part size, and production range flexibility. A supplier that does exclusively low-volume prototype work won't be set up for production quantities. A production shop may not have the responsiveness for rapid prototype iterations.
Multi-axis capability (4-axis, 5-axis) matters for complex automotive geometry. So does turning capability alongside milling. Ask what the shop's typical part complexity looks like and whether it's comparable to what you need.
Quality Control and Inspection
Understanding how a supplier controls quality throughout the process matters. CMM inspection capability for geometric verification, in-process gauging for critical features, first-article inspection processes, and traceability from material certs through to finished part documentation are all relevant.
For OEM automotive supply, quality management system certification (IATF 16949 for automotive-specific QMS, or ISO 9001 as a baseline) provides some confidence in systematic quality control. For aftermarket and motorsport supply, the specific inspection practices and their rigor matter more than formal certification.
Material, Finishing, and Engineering Support
Material availability matters for automotive machining. A supplier who regularly works with 7075-T6, 4140 steel, and titanium is better equipped to handle automotive work than one whose main experience is 6061. Surface finishing capability (anodizing, hard chrome, phosphate coating, zinc plating) in-house or through well-established relationships reduces lead time and coordination burden.
A supplier who can review a drawing and flag tolerance specifications that will drive significant cost increases, or identify geometry that would produce machining problems, saves real time and money versus one who simply machines whatever gets submitted.
Automotive CNC Machining FAQs
Q: What information should I provide when requesting an automotive CNC machining quote?
The CAD model defines the part geometry, but the drawing determines which dimensions and feature relationships are functionally important. Include the required material and quantity, along with any specified surface finish, heat treatment, or coating. The drawing should also show the applicable dimensional and GD&T requirements so the machining process and inspection method can be evaluated correctly. If the project requires CMM reports, FAI, material certification, or other customer documentation, state that with the RFQ rather than adding it after production starts.
Q: Can cast or forged automotive parts be CNC machined after forming?
Yes. CNC machining is commonly used to finish cast and forged automotive blanks when the forming process cannot hold the required feature accuracy by itself. Typical machined features include bearing bores, mounting interfaces, threaded holes, sealing surfaces, and other locations that determine assembly alignment. Using CNC only where precision is needed allows the casting or forging to provide most of the part geometry without machining the entire component from solid stock.
Q: When should an automotive part use 5-axis machining instead of 3-axis machining?
5-axis machining becomes useful when important features cannot be reached efficiently from a small number of fixed orientations. A part with angled ports, deep cavities, or features spread across several faces may require repeated setups on a 3-axis machine, increasing fixture changes and the risk of datum transfer errors. When the geometry can be machined accurately with fewer setups on a 5-axis machine, the higher machine capability can improve the overall process rather than simply adding cost.
Q: Do automotive CNC parts require CMM inspection or FAI documentation?
Not every automotive CNC part requires the same level of inspection or documentation. The requirement normally comes from the engineering drawing, customer quality requirements, control plan, and the characteristics being verified. CMM inspection is particularly useful when the drawing contains critical GD&T relationships or complex feature locations, while FAI documentation may be required when a customer needs formal evidence that the first production part conforms to the design requirements.
Q: Should I specify the required tolerance or fit class for a bearing bore?
Yes. A bearing bore should not be specified only as a generic "tight tolerance." The drawing should define the nominal diameter and the required fit or dimensional limits, and any applicable geometric controls should reference the correct datum structure. Where the bearing manufacturer specifies a particular housing fit or tolerance class, that requirement should be carried into the part drawing so the machining and inspection plan can be based on the actual bearing application.
Precision CNC Machining Service
Professional manufacturing, fast turnaround, and quality assurance.
Conclusion About Automotive CNC Machining
CNC machining for automotive components fills a specific and important role in vehicle manufacturing, not competing with casting or stamping for high-volume simple parts, but enabling prototyping, low-volume production, precision finishing, and the increasingly complex machined components that modern vehicle architectures require.
Understanding which automotive parts benefit from CNC machining, what processes and materials apply, and how tolerance requirements map to machining approach is the foundation for making good decisions about when to machine versus cast, forge, or stamp, and what to look for in a machining supplier when CNC is the right call.
JLCCNC supports CNC milling and turning for automotive prototypes, custom components, and low-volume production, with engineering review focused on geometry, tolerances, material selection, and manufacturability. Automotive drawings can be reviewed before production to identify features that require tighter process control or additional inspection.
Upload your CAD file and drawing to have the automotive part reviewed for machining feasibility, tolerance requirements, and production cost factors.
Popular Articles
• CNC Machining in the Medical Industry
• CNC for Luxury Watchmaking: Achieving Sub-Micron Tolerances
• Micro CNC Machining: Techniques for Manufacturing Miniature Components
• CNC Machining vs Sheet Metal: Which is Better for Enclosures?
• Micro CNC Machining Explained: Process, Precision & How Small It Can Really Get
Keep Learning
Custom Bicycle Parts: CNC Machining Guide
Key Takeaways CNC machining is often a practical choice for custom bicycle parts when production quantities are low, the geometry is complex, or critical interfaces require tighter dimensional control than near-net-shape forming can provide. The parts that benefit most are the ones where fit accuracy genuinely matters, such as bearing seats, bottom bracket interfaces, derailleur mounting features, and suspension pivots, where dimensional variation can affect assembly and performance. For CNC-machined ......
Online CNC Machining Services for Startups: Benefits & Uses
Key Takeaways Online CNC machining lets startups upload CAD files, get quotes, order custom parts, and manage production through a digital workflow. Prototyping: Startups can order single or small quantities to test fit, function, materials, and designs before scaling production. Production flexibility: The same CNC service can support prototypes, small batches, and higher quantities as product demand develops. Cost factors: Material, part size, geometry, tolerances, quantity, machining requirements, ......
CNC Machining for the Automotive Industry
Key Takeaways Automotive CNC machining is used both to produce certain low-volume components directly and to finish cast or forged parts at critical interfaces, including engine blocks, transmission housings, suspension uprights, brake components, and EV motor housings. CNC machining isn't how most automotive parts get manufactured in volume; casting, forging, and stamping handle the majority of mass production. What CNC does well is prototyping, low-volume production, precision finishing of cast or f......
CNC Machining for the Optics Industry: Optical Components & Housings
Key Takeaways CNC machining for optical systems primarily produces optomechanical components that hold, locate, align, and protect optical elements, including housings, lens barrels, mounts, spacers, retaining rings, and alignment fixtures. Conventional CNC machining is primarily used for the mechanical components around optical elements, while lenses and mirrors are generally produced through specialized grinding, polishing, coating, or ultra-precision machining processes. CNC machining provides the ......
Semiconductor CNC Machining: Precision Parts for Semiconductor Equipment
Key Takeaways CNC machining produces semiconductor equipment parts such as vacuum plates, manifolds, chambers, stages, brackets, and equipment housings. The function of a feature should set its machining requirements. A sealing surface needs suitable flatness and surface condition, while locating holes depend more on diameter and position. Large pockets can make an aluminum plate move after material removal. Roughing and finishing operations may therefore need separate setups. Thin walls can deflect u......
CNC Machining for Electronic Hardware: Design, Tolerances, and Manufacturing Considerations
(AI-generated) CNC milling of an aluminum electronics enclosure CNC machining plays a supporting but critical role in electronics manufacturing. While PCB fabrication creates traces, vias, and plated circuit features, CNC machining is used to produce the structural and mechanical parts that help the final device function reliably. What Is CNC Machining for Electronics CNC machining for electronics is the process of manufacturing high-precision mechanical parts used to support, protect, align, cool, or......