How Precise Is CNC Machining Compared To Other Manufacturing Methods?
11 min
- Tolerance, Accuracy, and Precision Aren't the Same Thing
- CNC Machining's Precision Range
- Comparison Across Manufacturing Methods
- Why CNC Machining Tends to Hold Tighter Tolerances
- Manual vs. CNC Machining Precision
- What Actually Determines CNC Machining's Achievable Precision
- A Common Misconception Worth Correcting
- Choosing Tolerances: Rules That Actually Generalize
- Quick DFM Rules to Lower Machining Costs
- FAQ
- Need Precision Machining for a Tight-Tolerance Project?
How Precise Is CNC Machining Compared to Other Manufacturing Methods?
Quick Answer: CNC machining generally holds tighter tolerances than forming, casting, and most additive processes, because it removes material directly rather than relying on shrinkage, springback, or layer deposition. But "how precise" depends on the specific process variant, material, geometry, and inspection method — there's no single number that applies across an entire process category.
A part spec calls for a tolerance of ±0.05mm, and the question that actually matters isn't "is CNC machining precise" — it's "precise compared to what, and is that the right process for this part in the first place." Precision isn't a single number that applies uniformly across manufacturing; it varies enormously by process, and knowing where CNC actually sits relative to the alternatives is more useful than a vague claim that it's "very precise."
Precision CNC Machining Service
Professional manufacturing, fast turnaround, and quality assurance.
Tolerance, Accuracy, and Precision Aren't the Same Thing
These three terms get used interchangeably in casual conversation, but they describe different things, and mixing them up is where a lot of confusion about manufacturing "precision" actually starts:
- Tolerance is the allowable deviation stated on a drawing — the range a dimension is permitted to fall within and still be accepted. It's a specification, not a measurement of anything a machine actually did.
- Accuracy is how close a part's actual, measured dimension comes to its intended nominal dimension. A process can be accurate on average even if individual parts vary somewhat.
- Precision (often used alongside repeatability) is how consistent a process is when producing the same feature over and over — low spread between parts, whether or not that spread is centered exactly on the nominal dimension.
A process can be accurate but not very repeatable (parts average out correctly but vary a lot part-to-part), or repeatable but not accurate (very consistent, but consistently off-target — usually fixable with a calibration offset once identified). What most people mean when they ask "how precise is CNC machining" is really a mix of tight achievable tolerance plus good repeatability — which is the sense used through the rest of this article, but it's worth knowing these aren't strictly synonyms when reading a spec sheet or a supplier's capability claims.
CNC Machining's Precision Range
CNC machining, through direct, computer-controlled material removal, can typically achieve tolerances in the range of ±0.02–0.1mm for standard work, with high-precision setups capable of holding ±0.005–0.01mm or tighter under well-controlled conditions. This comes from a combination of computer-controlled motion (which reduces operator-introduced variability compared to manual work), rigid tooling, and — on well-maintained equipment — real-time feedback from encoders and scales that help compensate for thermal drift and mechanical error during the cut. It doesn't come from CNC being immune to variation altogether — see the factors section below.
Comparison Across Manufacturing Methods
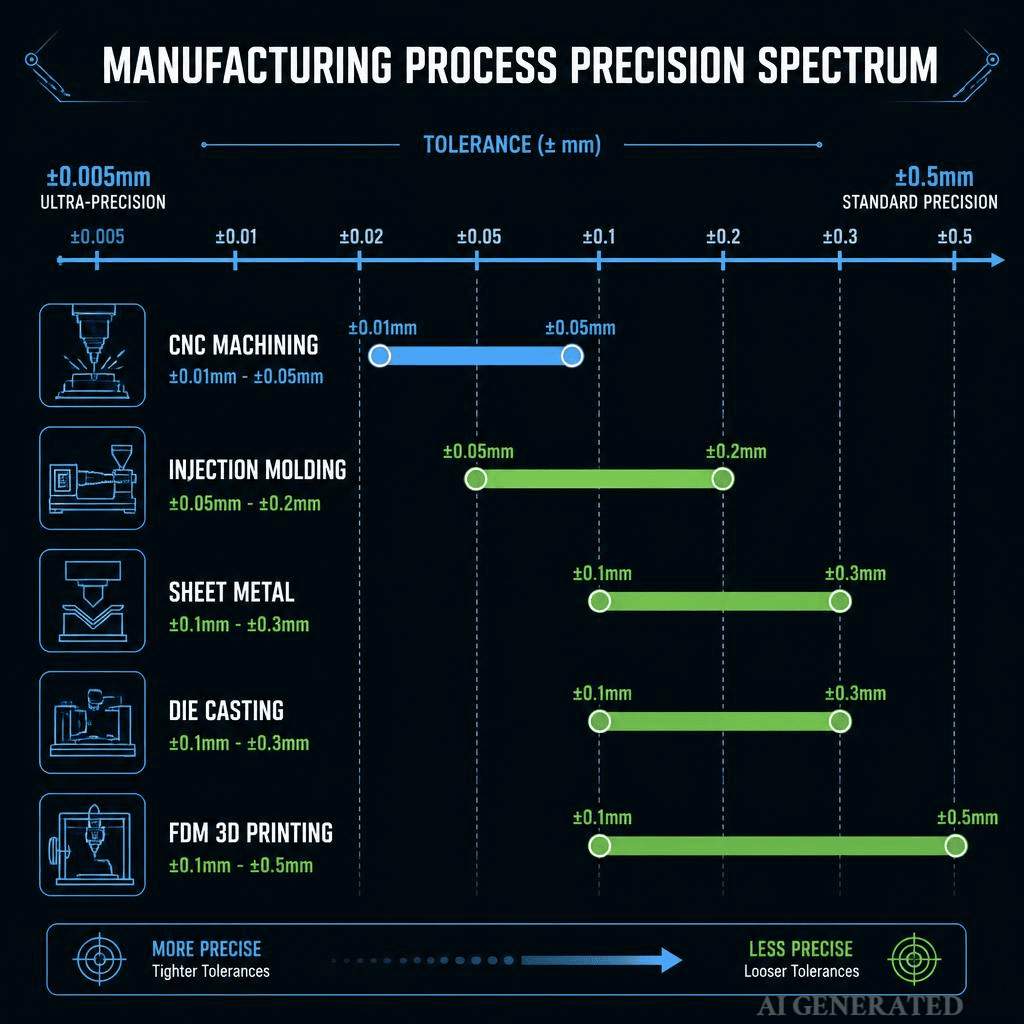
Typical as-produced ranges only; actual capability varies by material, part size, geometry, tooling, process control, and inspection method. These are not guarantees for any specific part or supplier.
| Process | Typical Tolerance | Why |
|---|---|---|
| CNC Machining | ±0.02–0.1mm (±0.005–0.01mm precision work) | Direct, repeatable material removal on critical features |
| Manual Machining | ±0.1mm and looser | Operator-dependent, no automated compensation across a run |
| Injection Molding | ±0.05–0.2mm, varies with part size and mold quality | Precision depends on mold tooling quality and material shrinkage as it cools |
| Die Casting | ±0.1–0.3mm typical | Molten metal shrinkage and mold wear; other casting types (sand casting, investment casting) vary more widely and are generally looser than die casting |
| Sheet Metal — Laser Cutting | ±0.05–0.15mm typical for the cut edge itself | Cutting accuracy is largely a function of the laser/beam and CNC control, closer to CNC's precision than bending is |
| Sheet Metal — Bending | ±0.1–0.3mm typical, tighter for the cut but looser once bent | Springback (elastic recovery after the bend) and tolerance stack-up across multiple bends add variation beyond the cut edge alone |
| 3D Printing — FDM | ±0.2–0.5mm typical | Layer resolution, nozzle diameter, and warping from uneven cooling |
| 3D Printing — SLA/DLP | ±0.05–0.15mm typical, tighter than FDM | Resin-based curing resolves finer layer detail than FDM's extruded filament, though still layer-built |
The relative ordering above holds fairly consistently — CNC machining sits among the tightest-tolerance processes available at reasonable cost — but the ranges genuinely overlap between adjacent processes (a well-controlled SLA print can outperform a poorly controlled CNC setup on a specific feature), so treat this as a general positioning guide, not a ranking where every CNC part beats every part from another process.
Why CNC Machining Tends to Hold Tighter Tolerances
The core reason isn't that CNC-cut material "doesn't introduce variation" — it still does, through tool wear, fixturing, cutting forces, thermal drift, and residual stress in the material, all of which a shop has to actively manage. The real structural advantage is that CNC machining can apply local, repeatable material removal and correction to specific critical features, rather than relying on a process that has to simultaneously control shrinkage, springback, or layer-to-layer variation across the whole part:
- Thermal Shrinkage in Molding/Casting: Injection molding and die casting rely on molten or semi-molten material flowing into a mold and then cooling — and that cooling process introduces shrinkage that varies with wall thickness, material, and cooling rate, a variable that has to be designed around in the tooling itself rather than corrected feature-by-feature.
- Springback in Sheet Metal: Sheet metal fabrication introduces its own variation through springback (the material's slight elastic recovery after bending) and the cumulative tolerance stack-up across multiple formed features.
- Layer Resolution in 3D Printing: 3D printing builds parts layer by layer, and that layered structure itself limits resolution and introduces potential warping as layers cool or cure at different rates.
None of this makes CNC machining universally "better" — each of these processes earns its place for reasons beyond precision alone (cost at volume, material properties, geometric freedom). But on tolerance specifically, CNC's ability to make targeted, repeatable cuts on the features that actually need it gives it a structural edge over processes that have to control shrinkage, forming, or layered deposition across the entire part at once.
Manual vs. CNC Machining Precision
Within machining specifically, CNC and manual approaches use the same fundamental cutting principles but differ in control. CNC's advantage over manual machining isn't that the cutting itself is inherently more precise in a single instance — a skilled machinist can hold tight tolerances on one part — it's that CNC significantly reduces the variability that comes from operator fatigue, inconsistency across a long run, and the physical limits of manually tracking multiple simultaneous axes. Manual machining's tolerance typically runs looser (±0.1mm and up) specifically because that operator-dependent variability is harder to control consistently across a production run, even when a single part can be made precisely by a skilled hand.
What Actually Determines CNC Machining's Achievable Precision
Beyond the process itself, several factors determine how tight a tolerance a specific CNC job can actually hold: machine rigidity and calibration, tooling quality and condition, material behavior (some materials hold tolerance more predictably than others, and residual stress in the raw stock can shift dimensions after cutting), programming and toolpath strategy, and — for genuinely tight-tolerance work — environmental control like temperature stability, since thermal expansion affects both the machine and the workpiece. A shop's general precision capability and a specific part's achievable tolerance aren't always the same thing; complex geometry or difficult materials can push a normally tight-tolerance shop's real-world capability looser than its best-case numbers suggest.
A Common Misconception Worth Correcting
Assuming the tightest tolerance a process can theoretically achieve is what a given part will actually get, without accounting for geometry and material, leads to both underspecifying critical dimensions and overspecifying ones that don't need it.
The tolerance ranges above are ceilings under favorable conditions, not defaults — a complex part in a difficult material won't automatically hit a shop's best-case tolerance figure just because that figure exists somewhere on a spec sheet.
Choosing Tolerances: Rules That Actually Generalize
Rather than anchoring on a specific number (like "±0.01mm for mating features, ±0.1mm for everything else") as a universal rule, the right tolerance for a given feature depends on:
- Function: Does this feature actually mate with another part, seal against something, or locate a precision component? If not, it usually doesn't need a tight tolerance regardless of what's achievable.
- Tolerance chain: How does this feature's tolerance stack up with the tolerances of the parts or features it interacts with? A tight tolerance on one feature can sometimes be relaxed if the chain it's part of has room elsewhere.
- Material: Some materials hold tight tolerances more predictably than others under the same process — this can shift what's realistic to specify.
- Part size and geometry: Larger parts and more complex geometry generally make the tightest tolerances harder to hold consistently.
- Inspection capability: A tolerance that can't be reliably measured with the inspection method actually available isn't a meaningful spec, regardless of what the machine could theoretically hold.
Quick DFM Rules to Lower Machining Costs
- Reserve tight tolerances for features that actually need them: Bearing seats, dowel pin holes, and critical sealing surfaces are common candidates — but the decision should follow function and tolerance-chain analysis, not a blanket "tightest tolerance for mating features" rule applied without checking whether that specific feature needs it.
- Default to standard commercial tolerances elsewhere: Looser, standard tolerances on non-critical features keep machine runtime lower and avoid unnecessary CMM inspection costs.
- Standardize chamfers and fillets: Avoid specifying sharp internal corners that force ultra-small cutters and increase tool deflection risk.
FAQ
Is CNC machining always more precise than 3D printing? Generally, for tolerance specifically — CNC's direct, targeted material removal typically holds tighter tolerances than layer-based 3D printing processes. But it depends on the specific 3D printing process (SLA/DLP resin printing generally holds tighter tolerances than FDM) and on how well-controlled the CNC setup actually is; 3D printing also offers geometric freedom, like complex internal structures, that machining can't easily replicate.
Why is injection molding generally less precise than CNC machining? Injection molding's precision is limited primarily by material shrinkage as molten plastic cools in the mold, which varies with wall thickness and material — a variable CNC machining's direct-removal process manages differently, though CNC has its own precision-limiting factors (tool wear, thermal drift, fixturing) that shift results depending on the specific job.
Can CNC machining achieve tighter tolerances than ±0.01mm? Yes, under well-controlled conditions with high-precision equipment, tight environmental control, and appropriate materials — though this level of precision typically comes with added cost and isn't the default capability of standard CNC work, and it depends heavily on the specific feature and material involved.
Does material affect achievable CNC machining precision? Yes — materials that machine more predictably (many aluminum alloys, for instance) tend to hold tighter tolerances more consistently than materials prone to work hardening, thermal distortion, residual stress, or inconsistent cutting behavior.
Need Precision Machining for a Tight-Tolerance Project?
Choosing the right tolerance for each feature — not just the tightest one available — is where cost and function actually get balanced. Our engineering team reviews your drawing before quoting, flags dimensions that may be over-specified, and confirms what's realistically achievable for your part's geometry and material.
- Multi-Axis Capability: Precision 3-, 4-, and 5-axis CNC milling and turning
- Engineering Review: Manufacturability and tolerance feedback with every quote
- Fast Quotes: Upload your 3D CAD files (.STEP / .IGES) for a rapid review and quote
Popular Articles
• What Steps Are Taken To Minimize Waste In CNC Machining Processes?
• Cutting with Precision: A Comprehensive Guide to CNC Water Jet Technology
• CNC Coolant Explained: Types, Maintenance & Safety
• Rake Angle in Machining: Machinists’ Guide to Perfect Cuts
• How EDM Wire Cutting Works: Complete Guide to Precision CNC Wire Cutting
Keep Learning
CNC Automation: Systems, Software, and Manufacturing Solutions Explained
Key Takeaways • CNC automation combines machine tools, software, and material handling into a system that reduces direct labor per part and improves process consistency. • The core components are the CNC machine, the control software, and whatever handles part movement, robot, conveyor, pallet system, or some combination. • Automation doesn't eliminate the need for skilled engineers and machinists. It shifts where their time goes, from operating machines to programming, setting up, and maintaining sys......
What Is Tempering? Metal Tempering Process and Applications
Key Takeaways In conventional quench-and-temper treatment, tempering reheats previously hardened steel below its lower critical temperature. Temperature and holding time affect the final mechanical properties. Tempered steel is used for tools, gears, shafts, and loaded components. CNC planning must account for heat-treatment distortion and final tolerances. Tempering differs from quenching, annealing, and normalizing in purpose and sequence. Tempering steel parts in an industrial furnace Hardening giv......
Sheet Metal vs CNC Machining: A Guide to Choosing the Right Method for Your Metal Parts
Sheet Metal vs CNC Machining: How to Choose the Right Method for Your Metal Parts Quick Answer: Choose sheet metal for uniform-thickness enclosures, panels, and formed brackets when bends and production volume support lower unit cost. Choose CNC machining for variable wall thickness, precision bores, tight feature relationships, and complex 3D geometry. Use a hybrid design when a formed structure needs precision-machined interfaces. A quote comes back for a bracket, and it's priced as a CNC part — mac......
How Precise Is CNC Machining Compared To Other Manufacturing Methods?
How Precise Is CNC Machining Compared to Other Manufacturing Methods? Quick Answer: CNC machining generally holds tighter tolerances than forming, casting, and most additive processes, because it removes material directly rather than relying on shrinkage, springback, or layer deposition. But "how precise" depends on the specific process variant, material, geometry, and inspection method — there's no single number that applies across an entire process category. A part spec calls for a tolerance of ±0.0......
CNC Milling vs. CNC Turning: Which is Better?
CNC Milling vs. CNC Turning: Which Process Fits Your Part? Quick Answer: Choose CNC milling for prismatic, flat, pocketed, and complex 3D parts. Choose CNC turning for parts whose primary geometry is cylindrical or rotationally symmetric. Use mill-turn or secondary milling when a turned part also needs flats, keyways, cross-holes, or other non-round features. A shaft and a bracket can come from the same material, hold similar tolerances, and still need completely different machines to make — not becau......
How Does CNC Machining Differ From Traditional Machining Methods?
How Does CNC Machining Differ From Traditional Machining Methods? Quick Answer: Choose CNC machining when repeatability, complex geometry, tight feature relationships, or production quantity justify programming and setup. Choose traditional or manual machining for simple one-off parts, repairs, and highly variable work where a skilled operator can work directly from a sample or drawing. The right choice depends on geometry, tolerance, quantity, and available data. A machinist trained on manual lathes ......