What Steps Are Taken To Minimize Waste In CNC Machining Processes?
10 min
- Waste Types and Where They Come From
- How to Measure Waste Reduction
- Lever 1: Design Optimization
- Lever 2: Material Management
- Lever 3: Strategic Machining (Toolpath and Process Planning)
- Lever 4: Tool Maintenance
- Lever 5: Waste Recycling
- How to Prioritize These Five Levers
- What Not to Compromise When Reducing CNC Waste
- FAQ
- Need Help Applying This to Your Part?
How to Reduce Waste in CNC Machining: 5 Practical Strategies
Quick Answer: CNC machining waste is reduced mainly through DFM, near-net stock, efficient toolpaths, preventive tool maintenance, and alloy-segregated recycling. The biggest gains usually come before cutting: reduce unnecessary material removal and prevent scrap or rework.
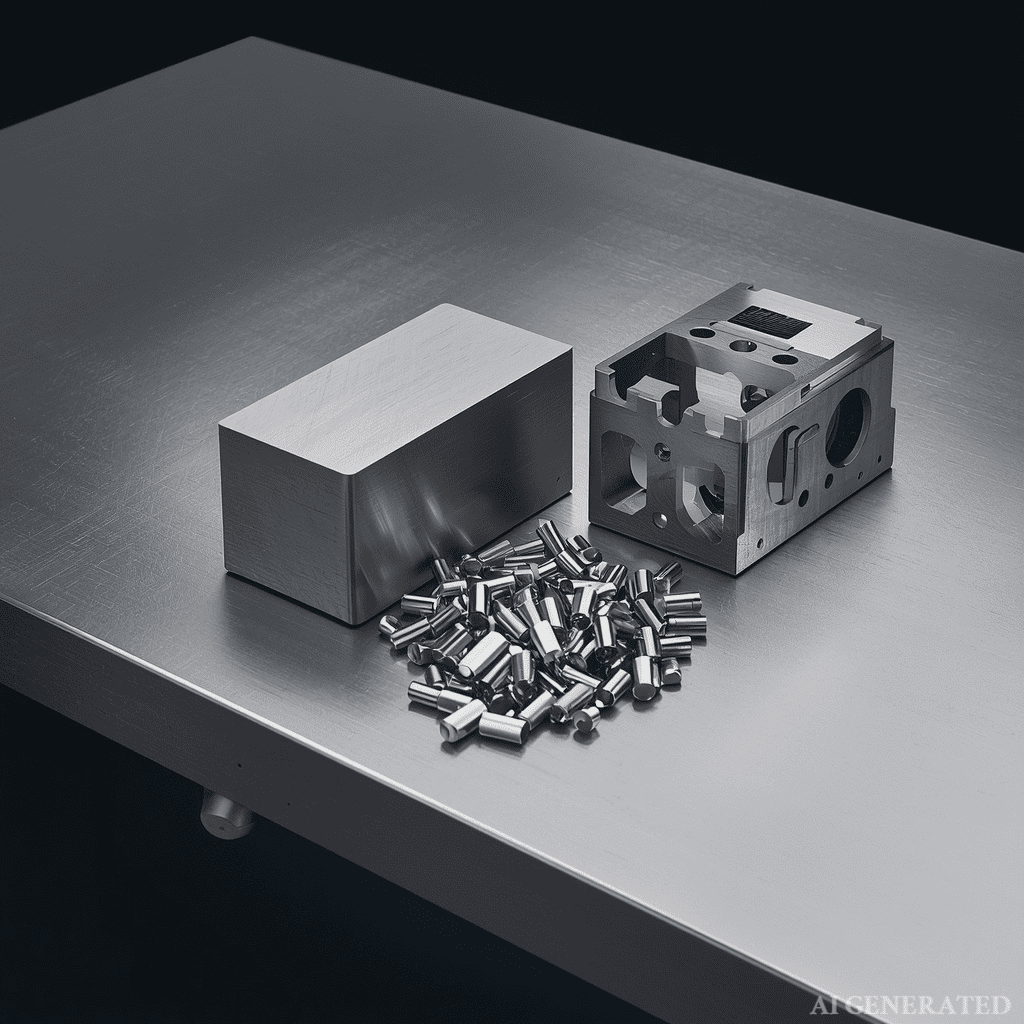
Every CNC-machined part starts as more material than it ends up being. A pocket gets milled out, a profile gets cut away, a boss gets faced down to size — and all of that removed material becomes waste, whether it's chips piling up in a bin or a block of expensive titanium reduced mostly to scrap. On some parts, the finished component is a small fraction of the raw stock's weight. Reducing that gap — without sacrificing the tolerances and finish a part actually needs — is less about any single trick and more about a handful of decisions made at different stages of the process, each with its own leverage.
This guide covers the five main levers that actually move the needle on CNC machining waste, with links to deeper guides on the ones that have enough depth to warrant their own dedicated articles.
Waste Types and Where They Come From
Waste in CNC machining isn't one thing — treating it as a single category makes it hard to know what to fix first. It splits into four distinct types, each with a different cause and a different fix:
| Waste type | What it is | Mainly addressed by |
|---|---|---|
| Unavoidable chips | Material removed as part of normal subtractive machining — the literal byproduct of cutting a shape from solid stock | Can't be eliminated, only recovered (Lever 5) |
| Avoidable excess stock | Material bought or left in the design beyond what the part actually needs — oversized billet, unnecessary wall thickness, stock faced away for no functional reason | Levers 1 and 2 (design and material management) |
| Scrap and rework | Parts that fail to meet spec, or that require reworking, due to tolerance drift, poor finish, or tool-related defects | Levers 3 and 4 (toolpath planning and tool maintenance) |
| Spent tooling and coolant | Worn cutting tools and used cutting fluid, treated as consumables but recoverable to a degree | Lever 5 (recycling and reconditioning) |
Some of this is close to unavoidable — chips are the literal byproduct of subtractive machining — and some is genuinely reducible through better decisions upstream of the actual cutting. The five levers below map onto the "mainly addressed by" column above.
Precision CNC Machining Service
Professional manufacturing, fast turnaround, and quality assurance.
How to Measure Waste Reduction
Before comparing levers, it helps to have a way to tell whether any of this is actually working. Three metrics cover most of it:
- Material utilization rate = finished part weight ÷ raw stock weight. This is the clearest single number for how much of what you bought ended up in the part versus the chip bin.
- Scrap / rework rate = number of parts scrapped or reworked ÷ total parts produced. Tracks the second waste type in the table above — quality-driven waste rather than design-driven waste.
- Alloy-segregated recycling recovery rate = value or weight of chips recovered by alloy type ÷ total chip volume generated. Reflects how much of the unavoidable chip waste is actually being recovered rather than landfilled or sold as low-value mixed scrap.
Tracking these turns "reduce waste" from a general goal into something a shop can actually measure improvement against.
Lever 1: Design Optimization
The cheapest waste to eliminate is the waste that never gets created in the first place, and design decisions made before a part ever reaches the machine have the biggest leverage on that. A part designed with excessive material where it isn't structurally needed gets machined down to size anyway — every bit of that unnecessary material becomes scrap. Reviewing a design specifically for material efficiency (not over-specifying wall thickness "to be safe," not adding stock that gets faced away for no functional reason) catches waste before it's ever cut. Our design for manufacturability guide covers this kind of review in more depth, including the broader set of DFM considerations beyond just material efficiency.
Lever 2: Material Management
How raw stock gets purchased, sized, and — where relevant — nested against a part's actual dimensions has a real effect on waste before machining even starts. Buying near-net-shape stock (raw material close to the finished part's dimensions) rather than machining a small part from an oversized block cuts waste dramatically on parts where that option exists.
Nesting specifically applies to sheet or plate stock and multi-part jobs — arranging multiple part outlines efficiently across a sheet to minimize the material lost between parts. It isn't a general CNC billet concept; a single part machined from a solid block doesn't have a "nesting" decision to make the way a batch of flat-pattern parts cut from a sheet does.
Material choice itself matters too, but the substitution logic has to run in the right order: the material still has to meet the part's performance requirements first. Only once a shortlist of materials clears that bar does it make sense to compare them on available billet sizes, how predictably each machines at the removal rates the job needs, and what the resulting chips are worth as segregated scrap. Swapping to a "more machinable" alloy that doesn't meet the part's actual requirements isn't a waste-reduction win.
Lever 3: Strategic Machining (Toolpath and Process Planning)
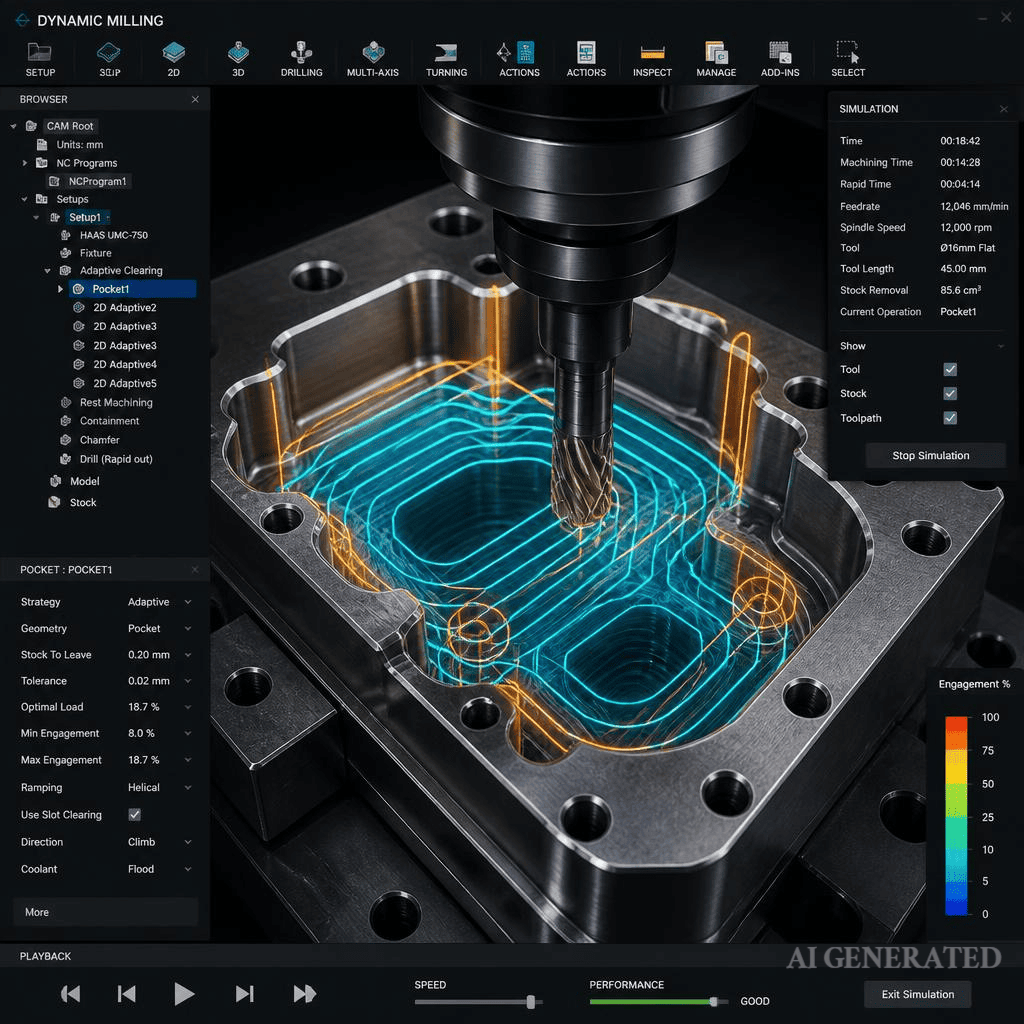
How the cutting itself is planned affects both direct material waste and the indirect waste from tool wear and rework. Efficient toolpath strategy — appropriate stepover, sensible roughing-to-finishing sequencing, avoiding unnecessary air-cutting or redundant passes — reduces both cycle time and the material removed less efficiently than it needs to be. Our guide on 5 CNC techniques to reduce waste in metal fabrication covers specific, actionable strategies at this level — smarter nesting, better blank sizing, intelligent toolpaths, optimized speeds, and simulation to catch problems before they become scrap.
Lever 4: Tool Maintenance
A dulling tool doesn't just cut less efficiently — it increases the risk of a part drifting out of tolerance or developing a poor surface finish, both of which can turn a nearly-finished part into scrap. Tracking tool wear against expected tool life, rather than running tools until they visibly fail, catches this before it produces bad parts. Our guide on tool wear detection and maintenance covers how to monitor this systematically rather than reactively.
Lever 5: Waste Recycling
What can't be avoided can often still be recovered. Metal chips have real scrap value and are commonly collected and recycled rather than landfilled — and for shops running enough volume, chip segregation by alloy meaningfully increases what that scrap is worth. Cutting fluid and coolant, often treated as a simple consumable, can be filtered, reconditioned, and reused rather than fully replaced on a fixed schedule. Our guide on zero-waste CNC strategies for recycling metal chips and coolant covers this specific piece of the waste picture — the recovery and recycling side, as distinct from the upstream prevention covered by the other four levers above.
How to Prioritize These Five Levers
Not every shop needs to tackle all five levers at once, and they aren't equally cheap to act on. A reasonable order to work through them:
- Check whether the billet or process itself can change first. Near-net-shape stock and process selection (Lever 2) are usually the single biggest lever available before any design or toolpath work happens.
- Then check whether the design is over-machining. A DFM review (Lever 1) catches unnecessary material and oversized stock allowances that would otherwise get machined away regardless of how efficient the toolpath is.
- Then reduce scrap and rework. Toolpath planning and tool maintenance (Levers 3 and 4) address the waste that comes from parts failing spec or requiring rework, which is often more expensive per part than raw material waste.
- Recover what's left. Recycling (Lever 5) is the last step because it deals with waste that's already unavoidable — chips and spent coolant that remain even after the first four levers are optimized.
This order roughly matches how much control each lever has upstream of the actual cutting — the earlier a decision happens in this list, the more waste it prevents rather than merely recovers.
What Not to Compromise When Reducing CNC Waste
Treating waste reduction as purely a sustainability or compliance concern, separate from cost, undersells how directly it affects the bottom line. Every gram of scrap material is raw material that was purchased and then paid for again in machine time to remove — waste reduction is a cost optimization lever as much as an environmental one, and in most shops, the cost argument is what actually drives adoption.
That said, waste reduction has a real failure mode worth naming directly: don't loosen functional tolerances, skip a necessary finishing pass, or lower a genuine quality requirement in the name of cutting material or cycle time. A part that comes back out of tolerance or fails in service because a step was cut to save material isn't a waste-reduction win — it's scrap with extra steps, and it usually costs more than the material it was meant to save. The "over-correcting" version of this mistake — tightening tolerances or adding excessive finishing passes in the name of "getting it right the first time" — is its mirror image, and can increase machining time and tool wear enough to offset whatever material savings were gained. Waste reduction works best as a set of deliberate, evaluated decisions at each of the five levers above — not a blanket instinct to cut corners, in either direction, everywhere at once.
FAQ
What percentage of raw material typically becomes waste in CNC machining? It varies enormously by part geometry, so there's no single figure worth quoting — a part machined from a mostly-solid block retains far more of the starting material than one with extensive pocketing or a complex profile cut from stock. The material utilization rate (finished part weight ÷ raw stock weight) is a more useful way to track this for a specific part than any general percentage.
Does reducing machining waste affect part quality? Not when done correctly — design optimization, better material sizing, and efficient toolpaths reduce waste without compromising the part's function. The risk is over-correcting in either direction (see the section above), where waste-reduction efforts start affecting tolerance or finish negatively, or excessive caution offsets the material savings gained.
Is scrap metal from CNC machining actually recyclable? Yes — metal chips and offcuts have real scrap value and are commonly collected and recycled, particularly when segregated by alloy type rather than mixed together, which affects the scrap's resale value.
What's the easiest place to start reducing CNC machining waste? Design review and material/stock selection tend to have the highest leverage relative to effort — catching unnecessary material or oversized stock allowances before a part is ever machined avoids waste that's much harder to recover once cutting has already happened.
Need Help Applying This to Your Part?
Need to reduce material removal or rework risk before production? Upload your CAD model and include material, quantity, critical tolerances, and finish requirements for a manufacturability-focused quote review. Every JLCCNC quote includes a DFM check, the same review covered in our design for manufacturing guide — so waste-related issues get flagged before a part is cut, not after.
Popular Articles
• What Steps Are Taken To Minimize Waste In CNC Machining Processes?
• Cutting with Precision: A Comprehensive Guide to CNC Water Jet Technology
• CNC Coolant Explained: Types, Maintenance & Safety
• Rake Angle in Machining: Machinists’ Guide to Perfect Cuts
• How EDM Wire Cutting Works: Complete Guide to Precision CNC Wire Cutting
Keep Learning
What Is Tempering? Metal Tempering Process and Applications
Key Takeaways In conventional quench-and-temper treatment, tempering reheats previously hardened steel below its lower critical temperature. Temperature and holding time affect the final mechanical properties. Tempered steel is used for tools, gears, shafts, and loaded components. CNC planning must account for heat-treatment distortion and final tolerances. Tempering differs from quenching, annealing, and normalizing in purpose and sequence. Tempering steel parts in an industrial furnace Hardening giv......
Sheet Metal vs CNC Machining: A Guide to Choosing the Right Method for Your Metal Parts
Sheet Metal vs CNC Machining: How to Choose the Right Method for Your Metal Parts Quick Answer: Choose sheet metal for uniform-thickness enclosures, panels, and formed brackets when bends and production volume support lower unit cost. Choose CNC machining for variable wall thickness, precision bores, tight feature relationships, and complex 3D geometry. Use a hybrid design when a formed structure needs precision-machined interfaces. A quote comes back for a bracket, and it's priced as a CNC part — mac......
How Precise Is CNC Machining Compared To Other Manufacturing Methods?
How Precise Is CNC Machining Compared to Other Manufacturing Methods? Quick Answer: CNC machining generally holds tighter tolerances than forming, casting, and most additive processes, because it removes material directly rather than relying on shrinkage, springback, or layer deposition. But "how precise" depends on the specific process variant, material, geometry, and inspection method — there's no single number that applies across an entire process category. A part spec calls for a tolerance of ±0.0......
CNC Milling vs. CNC Turning: Which is Better?
CNC Milling vs. CNC Turning: Which Process Fits Your Part? Quick Answer: Choose CNC milling for prismatic, flat, pocketed, and complex 3D parts. Choose CNC turning for parts whose primary geometry is cylindrical or rotationally symmetric. Use mill-turn or secondary milling when a turned part also needs flats, keyways, cross-holes, or other non-round features. A shaft and a bracket can come from the same material, hold similar tolerances, and still need completely different machines to make — not becau......
How Does CNC Machining Differ From Traditional Machining Methods?
How Does CNC Machining Differ From Traditional Machining Methods? Quick Answer: Choose CNC machining when repeatability, complex geometry, tight feature relationships, or production quantity justify programming and setup. Choose traditional or manual machining for simple one-off parts, repairs, and highly variable work where a skilled operator can work directly from a sample or drawing. The right choice depends on geometry, tolerance, quantity, and available data. A machinist trained on manual lathes ......
What Steps Are Taken To Minimize Waste In CNC Machining Processes?
How to Reduce Waste in CNC Machining: 5 Practical Strategies Quick Answer: CNC machining waste is reduced mainly through DFM, near-net stock, efficient toolpaths, preventive tool maintenance, and alloy-segregated recycling. The biggest gains usually come before cutting: reduce unnecessary material removal and prevent scrap or rework. Every CNC-machined part starts as more material than it ends up being. A pocket gets milled out, a profile gets cut away, a boss gets faced down to size — and all of that......