How Does CNC Machining Differ From Traditional Machining Methods?
8 min
- What "Traditional Machining" Means
- What CNC Machining Changes
- Direct Comparison
- Where CNC Machining Genuinely Wins
- Where Traditional Machining Still Makes Sense
- Cost and How to Choose
- A Common Misconception Worth Correcting
- FAQ
- Have a Part That Needs CNC Machining?
How Does CNC Machining Differ From Traditional Machining Methods?
Quick Answer: Choose CNC machining when repeatability, complex geometry, tight feature relationships, or production quantity justify programming and setup. Choose traditional or manual machining for simple one-off parts, repairs, and highly variable work where a skilled operator can work directly from a sample or drawing. The right choice depends on geometry, tolerance, quantity, and available data.
A machinist trained on manual lathes and mills can absolutely produce precise parts — plenty of skilled work still gets done that way. But hand someone a drawing calling for five hundred identical brackets, each holding a tolerance of a few thousandths of an inch, and the practical difference between CNC and traditional machining stops being academic. Both processes use fundamentally the same cutting principles — a tool removes material from a workpiece — but how that motion gets controlled changes almost everything else about what each is actually good for.

Precision CNC Machining Service
Professional manufacturing, fast turnaround, and quality assurance.
What "Traditional Machining" Means
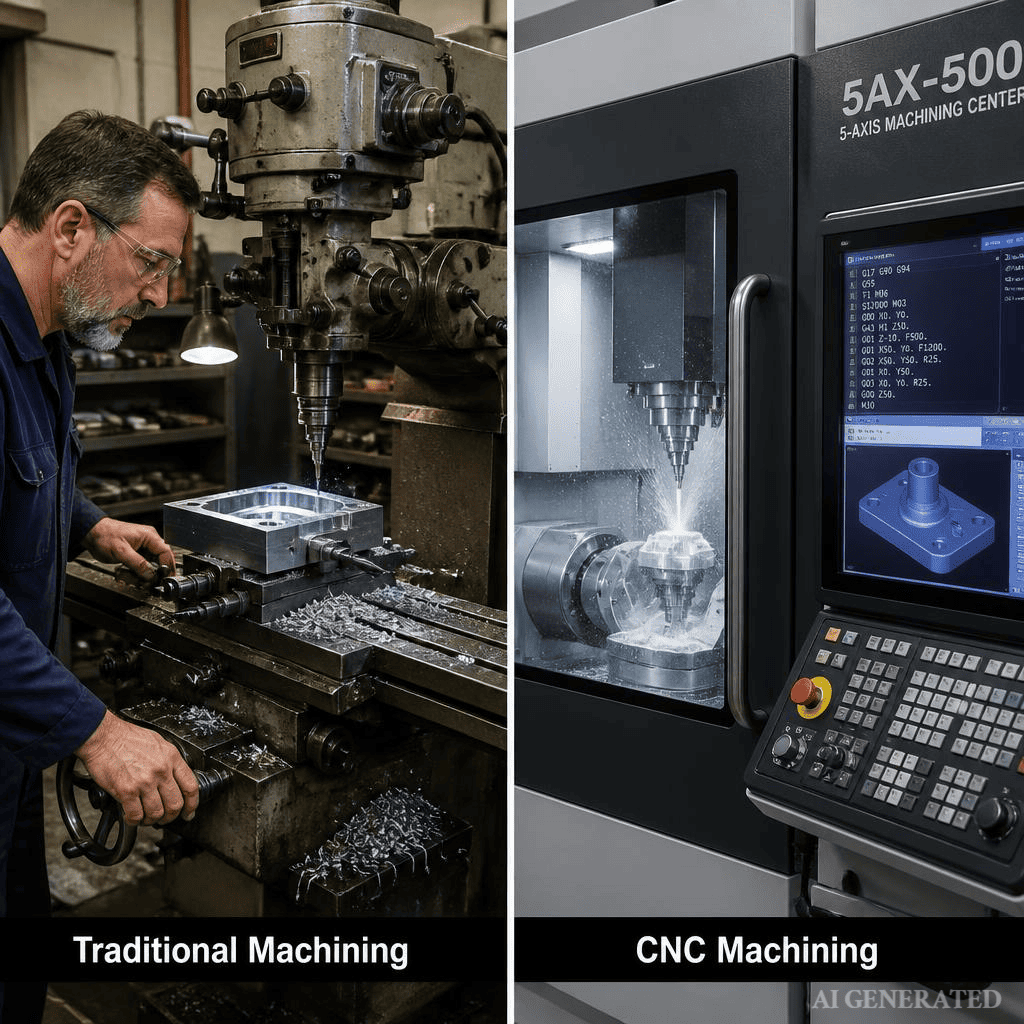
Conventional or traditional machining covers turning, milling, drilling, grinding, and sawing operations where a human operator directly controls the tool's motion — hand cranks, levers, and dials guiding the cut in real time, with the operator's skill and judgment determining accuracy. It's not an outdated or inferior process; it's a manually-controlled version of the same underlying material-removal principles CNC machining automates.
What CNC Machining Changes
CNC (Computer Numerical Control) machining replaces that manual control with pre-programmed instructions — a G-code program dictates exactly where the tool moves, how fast, and in what sequence, and the machine executes it without an operator adjusting the cut in real time. The core cutting physics are unchanged; what's automated is the control and repeatability of the motion.
Direct Comparison
| Factor | Traditional Machining | CNC Machining |
|---|---|---|
| Control | Manual, operator-guided | Computer-programmed |
| Repeatability | Varies with operator skill and fatigue | Consistent across a run — though still affected by tool wear, thermal drift, and fixturing over long runs |
| Typical tolerance | Around ±0.1mm and looser, operator-dependent | Tighter than manual work, commonly cited around ±0.01–0.05mm depending on equipment, material, and inspection — not a universal guarantee for any given shop |
| Setup time for a new part | Often faster for a single simple part | Requires programming, but reusable for repeat runs |
| Production speed | Bounded by operator pace per part | Faster per part once running, especially across a repeat batch |
| Cost structure | Closer to linear with labor time per part, no programming overhead | Upfront programming and setup cost that amortizes across the run |
| Best suited volume | One-off, low volume, highly custom work | Low volume through high volume production |
| Operator skill required | High — direct hands-on control | High, but different — programming and setup, not real-time cutting control |
| Complex geometry | Limited by what's practical to control manually | Handles complex 3D geometry reliably via CAM-generated toolpaths |
The tolerance figures above are typical reference ranges, not fixed capabilities of any specific machine or shop — actual achievable tolerance on either process depends on the equipment, workholding, tooling, material, and inspection method involved.
Where CNC Machining Genuinely Wins
Repeatability is the clearest advantage — a CNC program produces a much more consistent result on part 500 than it did on part 1, in a way manual machining struggles to match, since manual accuracy depends on operator consistency across an entire run and fatigue or attention lapses are a real factor at volume. That said, CNC doesn't eliminate variation entirely — it significantly reduces variation introduced by manual motion control, but tool wear, thermal drift in the machine and workpiece, and fixturing still affect a long CNC run and need to be managed with process controls and inspection, not assumed away.
Complex geometry that would be impractical to hold manually — coordinated multi-axis toolpaths, precise contoured surfaces — is typically impractical or uneconomical to produce by hand, since manually controlling that many simultaneous variables accurately at any consistent rate isn't realistic for most shops. Tight tolerances held consistently across a production run are also a CNC strength, since the process meaningfully reduces the operator variability that shows up run after run in manual work.
Where Traditional Machining Still Makes Sense
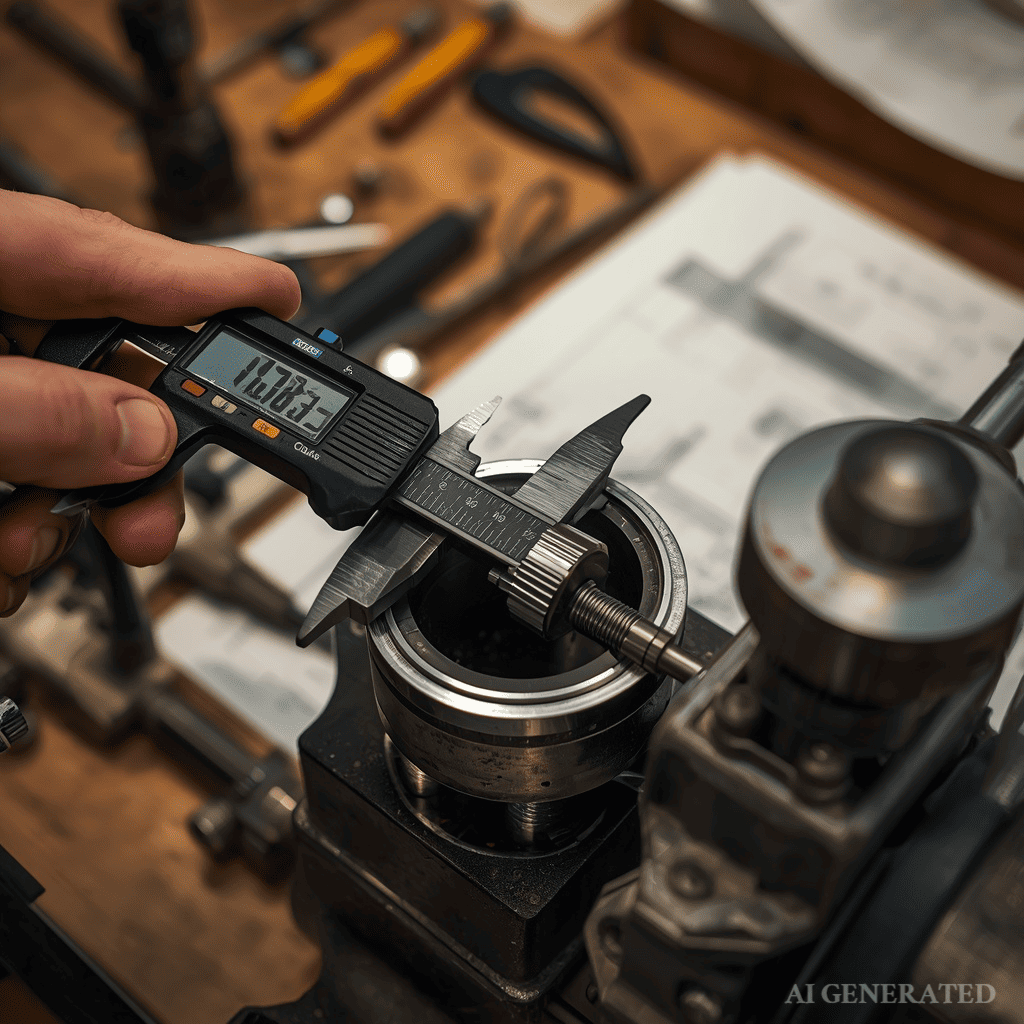
This is the part that often gets glossed over: traditional machining isn't simply an inferior, older version of CNC. For a genuine one-off part — a single custom fitting, a repair part with no digital file and no plan to make a second one — setting up and programming a CNC job can take longer than a skilled machinist simply cutting the part by hand. Small job shops and repair work, where the next job rarely resembles the last one, often favor manual equipment specifically because there's no setup or programming overhead to justify.
Highly experienced machinists can also make real-time adjustments mid-cut in response to how the material is actually behaving — reading chip formation, sound, and vibration — in a way that requires deliberate sensor-based process monitoring to replicate on a CNC setup. A worn-out part on decades-old equipment, with no CAD file and no plan to ever make a second one, is a common example — a skilled machinist measuring the original and cutting a replacement by hand is often faster and cheaper than modeling it, programming it, and verifying a CNC job for a single part that will never be ordered again. And for extremely simple features on a single part, the overhead of writing and verifying a CNC program can genuinely exceed just cutting it by hand.
Cost and How to Choose
CNC machining's upfront cost — programming, CAM work, first-article verification — doesn't pay off on a true one-off; it amortizes across a production run. Traditional machining's cost structure is closer to linear with labor time per part, without that upfront investment, but without CNC's scaling advantage either.
Exactly where the crossover sits between the two isn't a fixed quantity — it depends on how the specific job's programming time, fixturing setup, first-article verification, cycle time, labor rate, geometric complexity, and order quantity all combine. A simple part might favor traditional machining even at a moderate quantity if it's easy for a skilled machinist to hold by hand; a complex part can favor CNC even at very low volume, if manually holding that geometry's accuracy consistently would take a skilled machinist longer per part than programming and running it on a CNC machine. Rather than anchoring on a specific unit count, the more reliable approach is weighing those factors against the actual part and quantity in question — which is exactly what an engineering review before quoting is for.
A Common Misconception Worth Correcting
Framing this as CNC machining having simply "replaced" traditional machining industry-wide oversimplifies what actually happened. CNC dominates high-volume, high-precision, and complex-geometry production for good reason, but traditional machining hasn't disappeared — it persists specifically where its lack of setup overhead and real-time adjustability genuinely outperform CNC's strengths: true one-offs, repair work, and highly variable small-shop jobs. The right framing isn't "which one won," it's "which one fits this specific job's volume, complexity, and variability."
FAQ
Is CNC machining always more precise than traditional machining? Generally yes in terms of consistency across a run — CNC significantly reduces the variation introduced by manual motion control. A highly skilled machinist can achieve comparable precision on a single part manually, but holding that same precision consistently across many parts is where CNC's advantage becomes clear.
Is traditional machining cheaper than CNC for small jobs? Often, for a true one-off or very low quantity — CNC's programming and setup overhead doesn't amortize on a single part the way it does across a production run, and a skilled machinist can sometimes cut a simple one-off part manually faster than programming and verifying a CNC job for it. There's no fixed quantity where this flips; it depends on the part's complexity and the specific job's setup requirements.
Do machinists still need to learn traditional machining skills if CNC is more common? Many shops consider it valuable — understanding manual machining builds an intuitive sense of cutting forces, tool behavior, and material response that translates into better CNC programming and troubleshooting, even for machinists who primarily work on CNC equipment.
Can traditional machining achieve the same complex geometry as CNC? Not reliably for genuinely complex 3D geometry — coordinating multiple simultaneous axes accurately by hand isn't practical the way a CNC program executes it. Traditional machining is better suited to simpler geometry where manual control is sufficient to hold the required accuracy.
Have a Part That Needs CNC Machining?
For a production run, a complex geometry, or anything needing tight tolerances held consistently across multiple parts, CNC is generally the more practical route — and getting a clear picture of cost and feasibility starts with an actual quote against your design.
- Engineering Review: Manufacturability feedback with every quote
- Multi-Axis Capability: 3-, 4-, and 5-axis CNC milling for complex geometry
- Fast Quotes: Upload your 3D CAD files (.STEP / .IGES) for a rapid review and quote
Keep Learning
What Are Secondary Operations in Manufacturing?
Key Takeaways Secondary operations refine a part after its main production stage. Their classification depends on the production route. Typical tasks include machining, heat treatment, finishing, joining, and marking. Final drawing requirements help determine which added steps are needed. Extra stages can influence cost, lead time, handling, and inspection. Secondary operations are additional manufacturing steps performed after an earlier production stage to bring a part to its required final conditio......
What Is EDM? How Electrical Discharge Machining Works
What Is EDM (Electrical Discharge Machining)? How It Works & Applications A mold shop needs to cut a cavity into hardened tool steel — the kind of material that would dull a carbide end mill before the cut is even halfway done. A medical device maker needs a slot 0.05mm wide in a titanium component, thinner than most drill bits can even produce. Neither job is solvable with a spinning cutting tool, because the material is either too hard, the geometry too fine, or both. That's the gap EDM was built to......
Wire EDM Machine: Types, Specs & How to Choose One
Wire EDM Machine: Types, Specs & How to Choose One Our guide on how EDM wire cutting works covers the process itself — the spark erosion, the dielectric fluid, the tolerances the technique can hold. This one is about the machine that runs that process: what actually differentiates one wire EDM machine from another, and what matters when you're evaluating or specifying one. 💡 Need Precision Wire EDM Services? Understanding machine specs is crucial, but actually running them takes experience. At JLCCNC......
Titanium CNC Machining: Properties, Challenges & Best Practices
Titanium CNC Machining: Properties, Challenges & Best Practices A shop that's comfortable machining aluminum all day can still get caught off guard the first time a titanium job comes through. The part looks the same on the CAD screen, the toolpath strategy looks reasonable, and then the tool overheats, work-hardens the surface it just cut, and the finish comes out nothing like what aluminum would have produced at the same settings. Titanium isn't just "harder aluminum" — it behaves differently enough......
High Volume CNC Machining: What Changes When You Scale Production
High Volume CNC Machining: What Changes When You Scale Production Ten prototypes and ten thousand production parts are not the same problem wearing different clothes. A process that works fine for a handful of pieces — a bit of manual deburring here, a quick visual check there, tooling that gets swapped whenever it feels a little dull — falls apart the moment volume multiplies by a thousand. High volume CNC machining isn't just "the same thing, more of it." It's a different set of priorities, where de......
PTFE CNC Machining: Properties, Applications & Best Practices
PTFE CNC Machining: Properties, Applications & Best Practices PTFE — better known by the DuPont trade name Teflon — is a strange material to put on a CNC machine. It's soft, it barely holds a sharp edge itself, and it deforms under clamping pressure in ways that would ruin tolerance on almost any other engineering plastic. And yet it gets machined constantly, because nothing else offers PTFE's combination of an almost unbelievably low coefficient of friction and near-universal chemical resistance. Mac......