First Article Inspection: Process, Report & Requirements
10 min
- What Is First Article Inspection (FAI)?
- When Is First Article Inspection Required?
- How Is First Article Inspection Performed?
- What Is Included in a First Article Inspection Report?
- How Is FAI Applied to CNC Machined Parts?
- FAI vs. Other Manufacturing Inspections: What Is the Difference?
- What Is AS9102 and How Does It Relate to FAI?
- FAI FAQs
- Conclusion: First Article Inspection in Manufacturing
Key Takeaways
- FAI verifies an initial production item against defined requirements.
- Its scope may cover dimensions, materials, processes, and records.
- New parts or production changes can trigger an FAI.
- The report records objective evidence of product conformity.
- CNC parts may require GD&T, finish, material, and dimensional verification.
- Aerospace programmes may use AS9102 for structured FAI documentation.
When a first article inspection is required, the initial production part is evaluated against the applicable engineering and manufacturing requirements before the results are accepted for the intended production use. The exact timing and scope depend on the customer, contract, industry requirements, and quality system.
What Is First Article Inspection (FAI)?
First Article Inspection (FAI) is a formal, documented verification that a production part conforms to the applicable engineering drawing, specifications, material and process requirements, and customer requirements. A first-piece inspection may be a limited setup or dimensional check, while FAI provides documented verification of the applicable design characteristics and supporting product requirements. The results are documented in a First Article Inspection Report (FAIR), providing traceable evidence of the characteristics that were verified.
For CNC parts requiring FAI, JLCCNC can review the drawing and inspection requirements before machining to define the appropriate inspection scope and documentation.

Precision CNC Machining Service
Professional manufacturing, fast turnaround, and quality assurance.
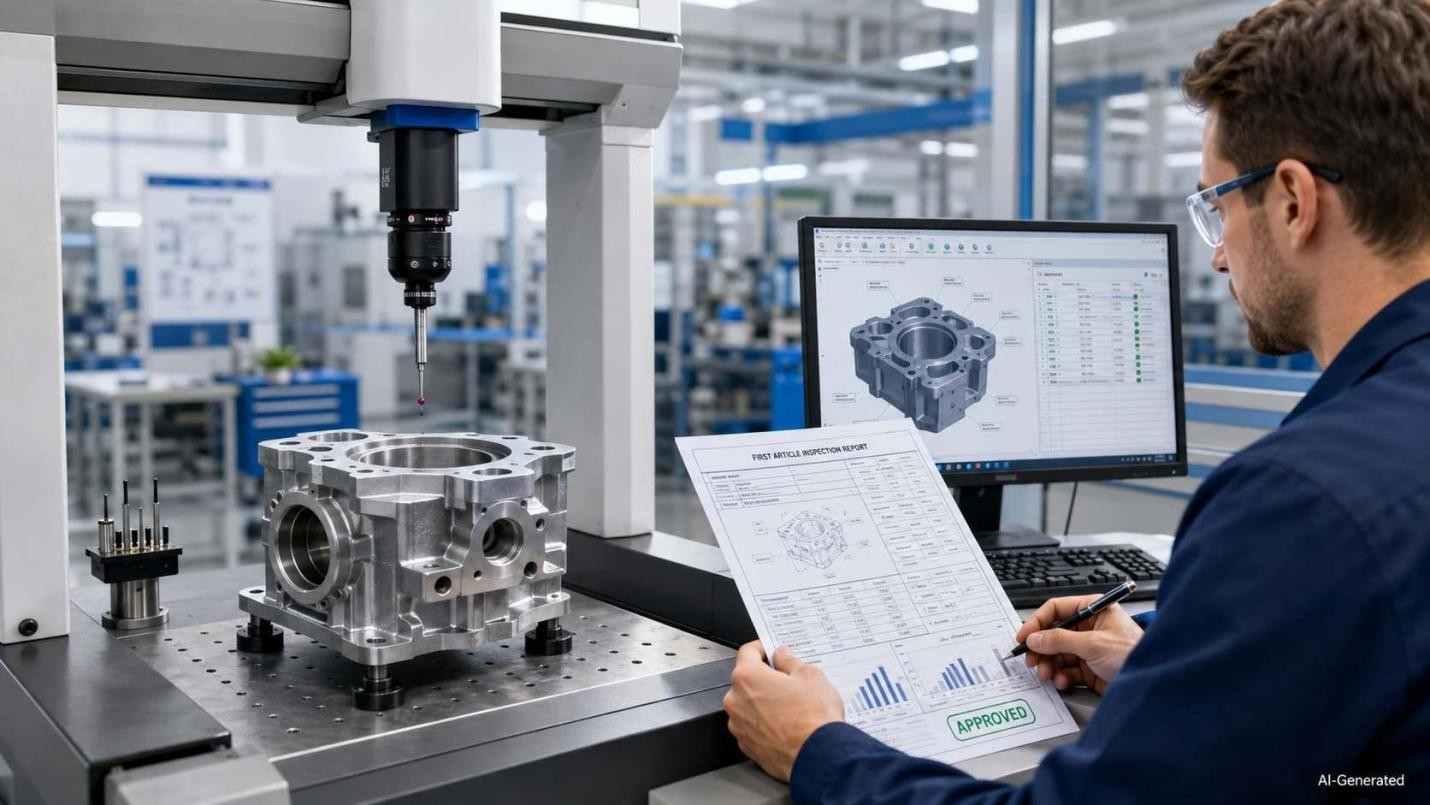
First article inspection of CNC machined parts
Why Is First Article Inspection Important in Manufacturing?
FAI can expose drawing-interpretation, tooling, setup, or manufacturing issues before they are repeated across a larger production run. This can reduce the risk of avoidable scrap, rework, and production delays. It also supports informed release decisions across engineering, quality, production, and customer teams before routine manufacturing proceeds.
When Is First Article Inspection Required?
New Parts or New Production Processes
A new part may require FAI before routine production moves ahead, depending on the customer, contract, industry requirements, and applicable quality system.
Design, Process, or Tooling Changes
An engineering revision, manufacturing-process change, tooling change, material change, or other change that affects previously verified product characteristics may require a full or partial FAI. The required scope should be determined from the applicable customer and quality requirements. For aerospace programs, the applicable FAI procedure should be used to determine whether the change requires a full or partial FAI and which characteristics must be re-evaluated.
Production Changes or Customer-Specified Triggers
Depending on the governing requirements, additional triggers may include a change of manufacturing source or location, an extended production interruption, or a customer request for renewed verification. Such kinds of situations are not governed by one universal rule. This makes the governing contract, specification, and quality procedure the final reference for each program.
How Is First Article Inspection Performed?
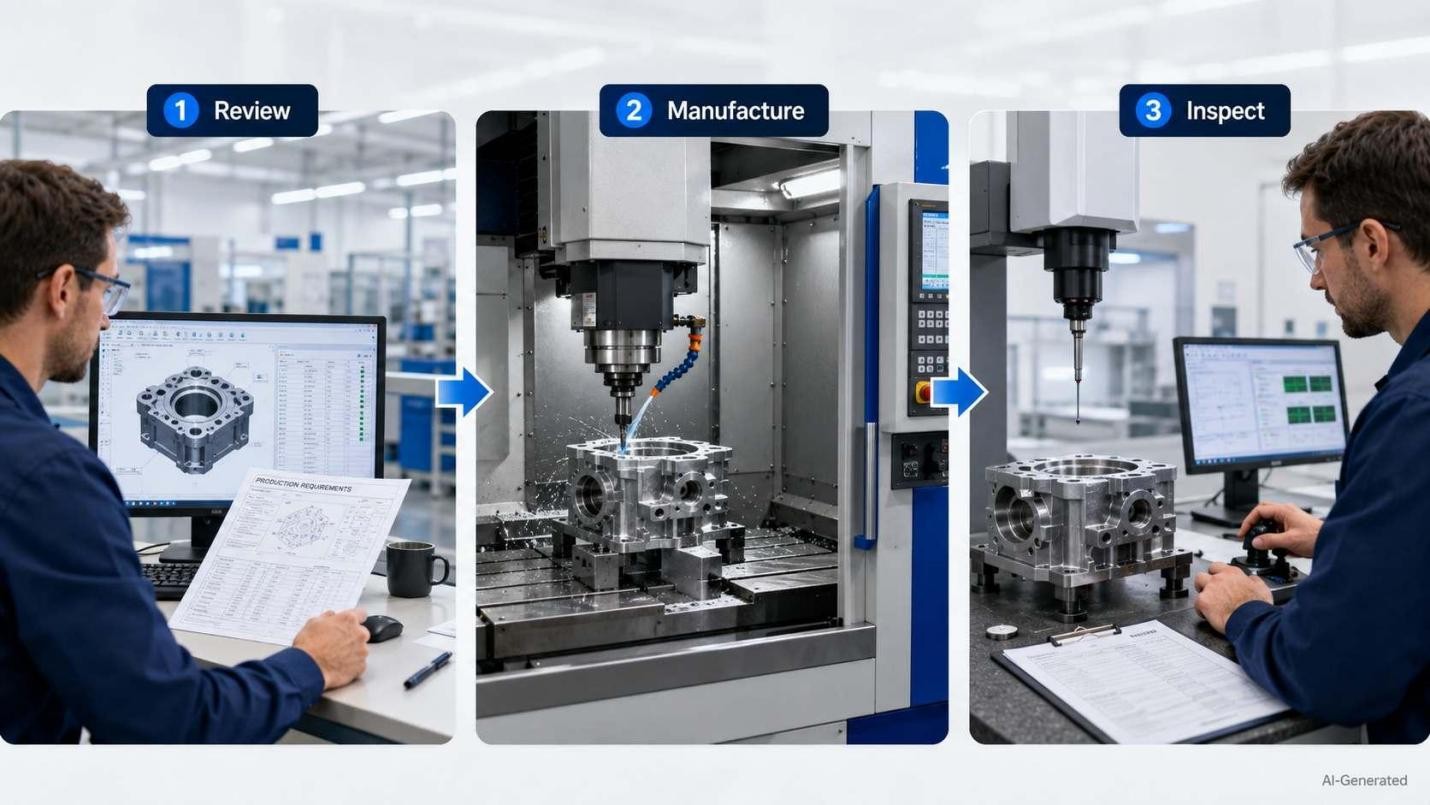
First article inspection process from review to inspection
Review the Drawing and Production Requirements
The process begins by gathering the current drawing revision, specifications, purchase order terms, material requirements, and manufacturing instructions. The inspection team identifies the design characteristics on the current drawing or digital product definition, typically using a ballooned drawing or equivalent characteristic numbering system. Each characteristic is then assigned a reference number and linked to its requirement, inspection method, and recorded result. For aerospace FAI, SAE revised AS9102 to Revision C on June 28, 2023.
Manufacture the First Article Under Production Conditions
The first article should be produced using the intended manufacturing process, equipment, tooling, materials, and work instructions. This allows the inspection results to represent the actual production route rather than a special one-off setup.
Inspect, Document, and Review the Results
Once the part is ready, required characteristics are examined, and the results are captured in the first article inspection report with supporting evidence that is required by the governing procedure. Quality personnel review the completed package, address any nonconformance, and decide whether or not further action or renewed inspection is needed before the FAI is closed.
What Is Included in a First Article Inspection Report?
Part and Drawing Information
A report identifies the part number, part name, serial number, drawing number, revision level, and related assembly or manufacturing references. These entries tie the inspected item to the exact product configuration under review. It avoids linking results to the wrong revision. AS9102C Form 1 contains 26 numbered data fields covering part identification, revision, manufacturing references, FAI status, and approval information.
Material, Process, and Supporting Documentation
The FAI report also records applicable material specs, certificates, special processes, and functional test references that are required. Supporting records can include material certifications, process approvals, or laboratory evidence. The exact format depends on customer instructions, contract terms, and any governing standard.
Dimensional and Other Inspection Results
For each applicable characteristic, the report records the requirement, the inspection result, and other traceability information required by the governing procedure. Depending on the characteristic, this may include the inspection method, qualified tooling, or a referenced nonconformance record. It allows reviewers to identify conformity or any nonconformance that demands follow-up.
How Is FAI Applied to CNC Machined Parts?
For a CNC-machined housing, for example, the FAI may trace critical bore diameters, hole locations, datum relationships, material certification, and surface requirements back to the drawing characteristics. The inspection method is selected according to the characteristic and its tolerance rather than using the same instrument for every dimension.
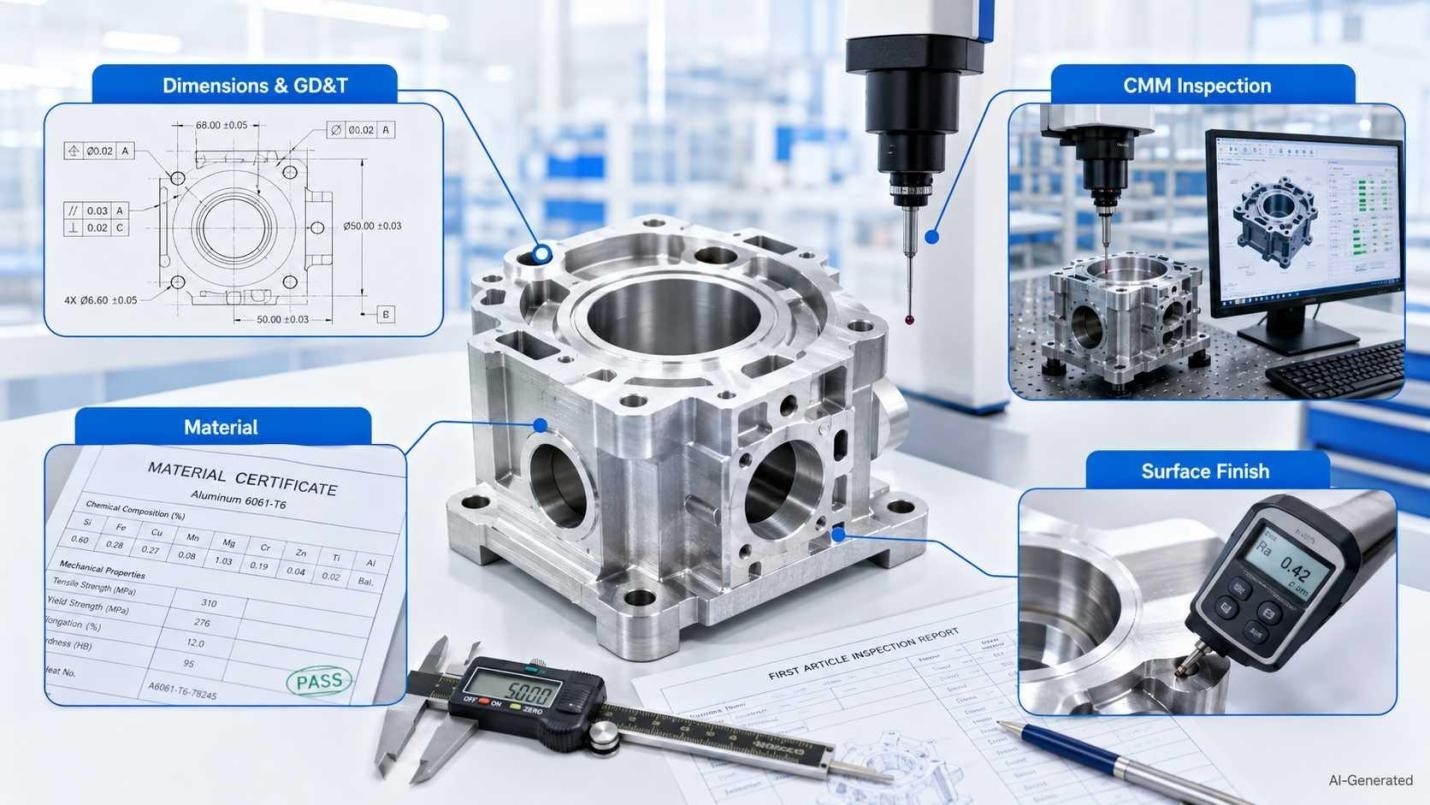
FAI inspection of CNC machined part and key features
Dimensions, Tolerances, and GD&T
For CNC machined parts, FAI typically verifies the dimensional and geometric characteristics defined on the drawing, including critical hole locations, bore sizes, thicknesses, datum relationships, and GD&T controls. The inspection results are linked to the corresponding drawing characteristics.
GD&T requirements can cover form, orientation, location, profile, and runout in relation to defined datums. ASME Y14.5-2018 was reaffirmed in 2024 and is currently designated Y14.5-2018 (R2024).
Material and Surface Finish Requirements
Just dimensional conformity is not sufficient in FAI manufacturing. Material grade and condition can be supported by certification records. Specified surface texture may require measurement with instruments such as a profilometer. Surface requirements should follow the parameters and symbols that are stated in the technical documentation.
Critical Features and Measurement Methods
Features that affect fit, function, or assembly may require particular attention during FAI. Examples include precision bores, threads, datum surfaces, hole patterns, sealing faces, and tightly controlled locations. The inspection method should match the characteristic and its tolerance. Micrometers, bore gauges, thread gauges, optical systems, and CMMs may be used depending on the feature and the required measurement.
A CMM is particularly useful for complex geometry and relationships between multiple features, especially when they must be evaluated from a common datum reference frame. Dedicated gauges or other instruments may be more suitable for features such as threads or surface texture.
FAI vs. Other Manufacturing Inspections: What Is the Difference?
| First Article Inspection (FAI) | First-Piece Inspection | Final Inspection | Routine or In-Process Inspection | |
|---|---|---|---|---|
| Primary purpose | Verify that an initial production item conforms to the applicable product requirements and that the required production evidence has been documented. | Check an early part from a production run to confirm the setup is producing acceptable output. | Confirm the completed product meets specified acceptance requirements before releasing or shipment. | Monitor selected characteristics during production and detect variation before the affected parts move to later operations or final release. |
| Standard timing | At the first production run and after qualifying changes. | At the beginning of a run, setup, or production change. | After manufacturing operations are complete. | At defined stages while production is underway. |
| Scope | Broader, covering applicable design characteristics and supporting production evidence. The required extent depends on the governing requirement. | Limited to selected dimensions, features, or setup checks linked to starting production. | Covers the acceptance criteria that is assigned to final product verification. | Targets selected characteristics for ongoing process control, such as critical dimensions or other controlled process outputs. |
| Documentation | May require a formal FAIR with structured records. Aerospace applications using 9102 have defined documentation requirements. | Recorded on an inspection sheet, setup record, or internal quality document. | Recorded through final inspection results, release records, or other required quality documentation. | Records include inspection logs, control-plan entries, and statistical process data. |
| Terminology note | The meaning may be governed by a customer, contract, industry standard, or internal quality system. | Some manufacturers use first-piece and first article differently. Others may use the terms more loosely. | Scope and naming can differ according to the manufacturer and industry. | Terms such as in-process, patrol, stage, or routine inspection may describe related activities depending on the quality system. |
What Is AS9102 and How Does It Relate to FAI?
How AS9102 Structures FAI Documentation
AS9102C is an aerospace standard that establishes requirements for performing and documenting FAI. FAI is the verification activity. AS9102C defines requirements for how that activity is performed and documented in applicable aerospace supply chains.
What Are AS9102 Forms 1, 2, and 3?
AS9102C organizes FAI documentation into three forms, each covering a different part of the accountability and verification record.
| AS9102C Form | Purpose |
|---|---|
| Form 1 | Part Number Accountability |
| Form 2 | Product Accountability — Materials, Special Processes, and Functional Testing |
| Form 3 | Characteristic Accountability, Verification, and Compatibility Evaluation |
When Does AS9102 Apply to FAI?
AS9102 is primarily used for aviation, space, and defense products. An organization outside these sectors may also adopt the standard as a customer or internal requirement. Where AS9102 applies, its requirements supplement rather than replace applicable customer, contractual, statutory, and regulatory requirements.
FAI FAQs
What Does FAI Stand For?
FAI stands for First Article Inspection. It refers to the documented verification of an initial production item against applicable requirements.
What Is an FAI Report?
An FAI Report, called a FAIR, records the product identification, applicable requirements, inspection evidence, measured results, and supporting documentation for the inspected item.
Does FAI Need to Be Approved Before Production?
Not in every case. Approval requirements depend on the customer, contract, purchase order, applicable industry requirements, and internal quality procedures.
Does Every New Part Require FAI?
No universal rule demands FAI for every new part. The obligation depends on contractual terms, customer needs, applicable standards, and the organization's quality system.
How Many Parts Are Needed for FAI?
The required quantity depends on the applicable customer or quality requirement. A single representative production part is common, but additional samples may be required for certain products, processes, or customer specifications.
What Happens If a First Article Inspection Fails?
The nonconforming characteristic should be documented and corrected through the applicable nonconformance process. Depending on the change or corrective action, a partial or full FAI may be required to re-verify the affected characteristics.
Conclusion: First Article Inspection in Manufacturing
FAI provides documented evidence of whether an initial production part conforms to the applicable drawing and manufacturing requirements. For CNC machining, inspection records can link drawing characteristics to measured results and provide traceability for the review. The required scope depends on the customer, contract, and applicable quality requirements.
Precision CNC Machining Service
For a CNC part that requires FAI, upload the drawing to JLCCNC to start the machining and inspection review.
Keep Learning
Laser Engraving Aluminum: Marking Methods & Surface Effects
Key Takeaways Laser engraving usually removes base material to create a recess. Laser marking is a broader term that can describe a surface-color change or material removal, so the process name alone does not define the final result. On aluminum, alloy and surface finish affect marking contrast. A light mark on dark anodized aluminum is a common design target, but the actual appearance depends on the finish and laser process. JLCCNC laser marking produces a recessed area 0.03–0.1 mm deep. The result i......
CNC Cutting Fluid: Types, Functions, Applications, and Selection Guide
Key Takeaways Cutting fluid in machining performs four functions simultaneously: cooling the tool and workpiece, lubricating the tool-chip interface to reduce friction, carrying chips away from the cut zone, and protecting machined surfaces from corrosion between operations. Different machining operations need different fluid priorities: high-speed aluminum milling may need adhesion control and chip evacuation, threading and tapping need strong lubrication, and grinding requires both cooling and fine ......
Blind Hole Machining Guide: What Is a Blind Hole, Types of Holes, and Tapping Tips
What Is a Blind Hole? Types of Holes and CNC Hole Machining Explained In CNC machining, few operations challenge process control and tool stability as much as blind hole machining. A blind hole is a hole that terminates at a defined internal depth rather than breaking through the opposite surface. Because the cavity is enclosed at the bottom, chip evacuation, thermal behavior, tool wear, and dimensional accuracy become far more difficult to manage compared to through-hole machining. These constraints ......
Rake Angle in Machining: Machinists’ Guide to Perfect Cuts
What is Rake Angle? (minaprem) If you've ever stood in front of a CNC machine or a manual lathe, you know that the cutting tool's geometry isn't just some arbitrary design. Every angle, edge, and surface has a job to do, and one of the most important of those is the rake angle. We've been running machines long enough to know that rake angle can make or break your surface finish, tool life, and machining efficiency. In this guide, we're going to walk you through what rake angle is, how it works, and ho......
Sheet Metal vs CNC Machining: A Guide to Choosing the Right Method for Your Metal Parts
Quick Answer: Choose sheet metal for uniform-thickness enclosures, panels, and formed brackets when bends and production volume support lower unit cost. Choose CNC machining for variable wall thickness, precision bores, tight feature relationships, and complex 3D geometry. Use a hybrid design when a formed structure needs precision-machined interfaces. A quote comes back for a bracket, and it's priced as a CNC part — machined from solid aluminum, a few hours of spindle time, a per-part cost that makes......
What Steps Are Taken To Minimize Waste In CNC Machining Processes?
How to Reduce Waste in CNC Machining: 5 Practical Strategies Quick Answer: CNC machining waste is reduced mainly through DFM, near-net stock, efficient toolpaths, preventive tool maintenance, and alloy-segregated recycling. The biggest gains usually come before cutting: reduce unnecessary material removal and prevent scrap or rework. Every CNC-machined part starts as more material than it ends up being. A pocket gets milled out, a profile gets cut away, a boss gets faced down to size — and all of that......