Drill and Tap Chart: Metric, UNC & UNF Tap Drill Sizes
13 min
- Introduction
- Quick Reference: Drill and Tap Chart
- What Is a Drill and Tap Chart
- How to Read a Drill and Tap Chart
- CNC Drilling and Tapping Process
- Factors Affecting Tap Drill Size Selection
- Common Drill and Tap Issues
- Drill and Tap Chart FAQs
- Conclusion About Drill and Tap Charts
Key Takeaways
- A tap drill chart gives the recommended starting hole size for an internal thread.
- Metric threads are identified by diameter and pitch, while UNC and UNF threads are identified by diameter and TPI.
- The tap drill diameter affects how much material remains for the tap to remove and therefore influences the resulting percentage of full thread and tapping load.
- The charts cover commonly used metrics, UNC, and UNF threads in CNC machining.
Introduction
An internal thread starts with a drilled hole. The hole must be large enough to limit tapping load while leaving sufficient material for the tap to form the required thread profile.
The required drill diameter changes with the thread specification. For example, M6 x 1.0 has a different tap drill requirement from M8 x 1.25. This is the same for inch threads: 1/4-20 UNC and 1/4-28 UNF have the same nominal diameter but different thread pitches, so their starting hole sizes are different.
This guide explains:
- Internal threads: Common metric, UNC, and UNF tap drill charts.
- How to accurately read thread size, pitch, TPI, and tap drill reference.
- The typical aspects of drilling, tapping, and checking threaded holes in CNC machining.
Quick Reference: Drill and Tap Chart
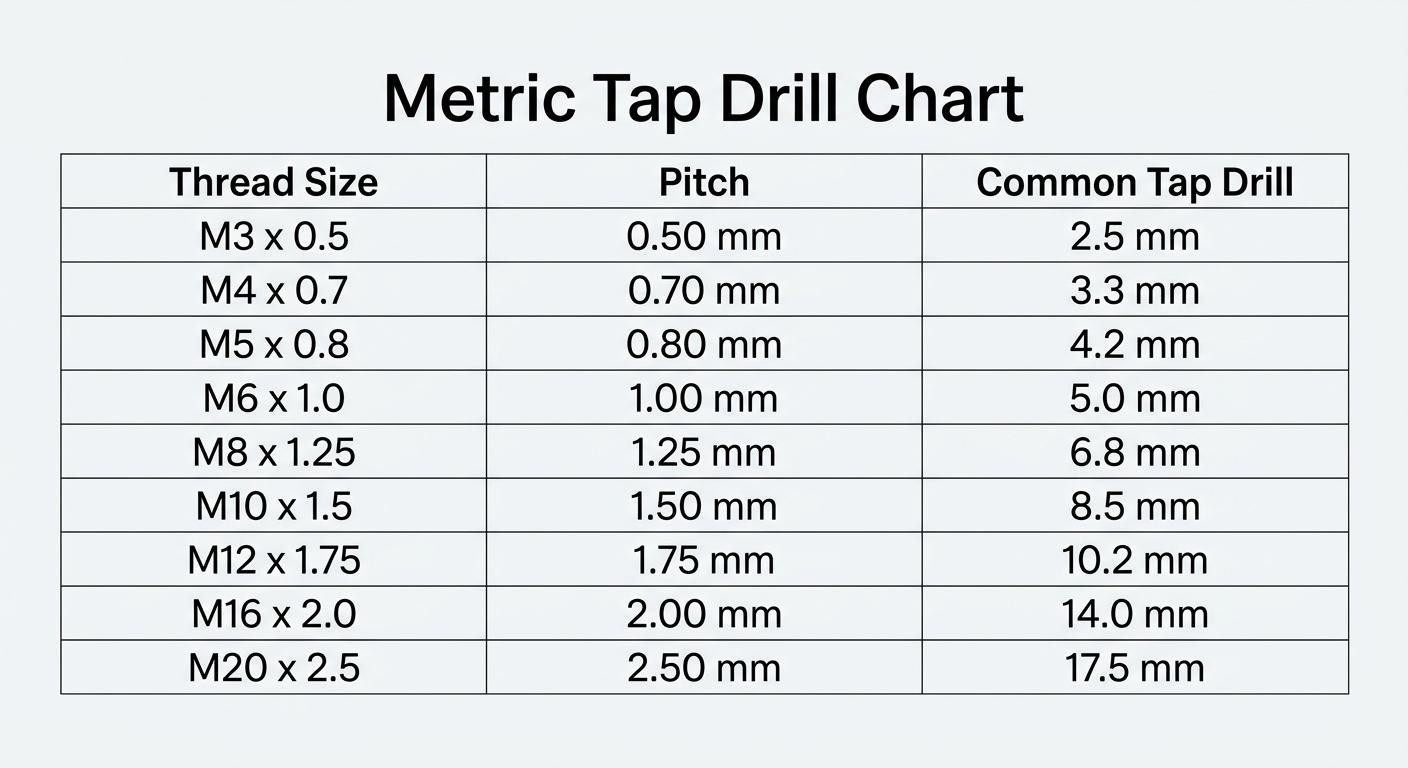
A tap drill chart gives the starting hole diameter for cutting an internal thread. The values below are common starting sizes for conventional cutting taps. Actual drill size may vary with the target percentage of thread, thread class, workpiece material, tap geometry, and manufacturer recommendations. For production work, use the tap manufacturer's specified drill range as the final reference.
A tap drill is smaller than the nominal thread diameter because material must remain for the tap to form the internal thread. For example, an M6 x 1.0 cutting-tap hole commonly starts at 5.0 mm, while a 1/4-20 UNC hole commonly starts with a #7 drill. Actual production drill selection should follow the specified thread class and the tap manufacturer's recommendation.
Metric Tap Drill Chart
UNC Tap Drill Chart
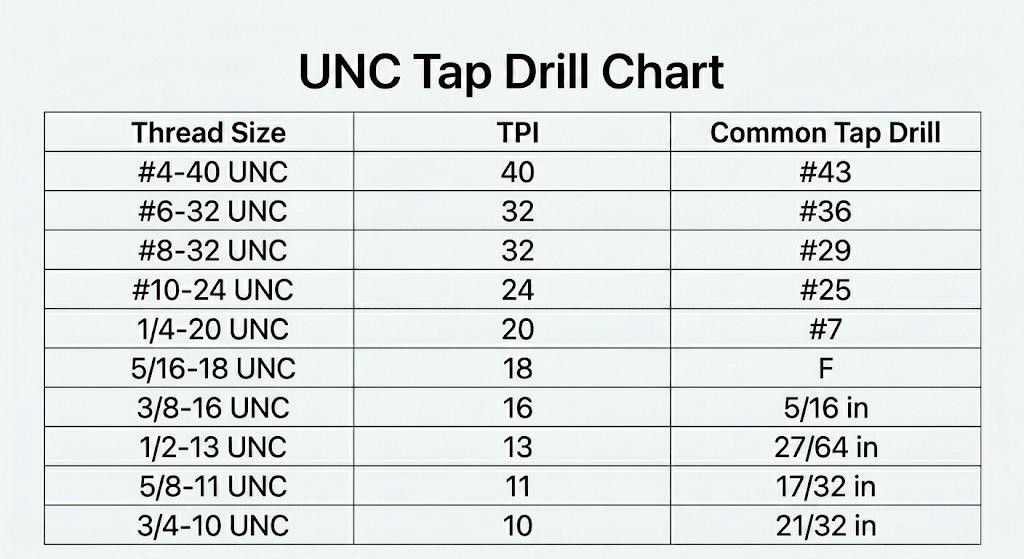
Tap drill size may vary with the target percentage of full thread, internal thread class, workpiece material, tap type, and the tap manufacturer's recommendations. The sizes above are common starting points for standard UNC tapping.
UNF Tap Drill Chart
Note
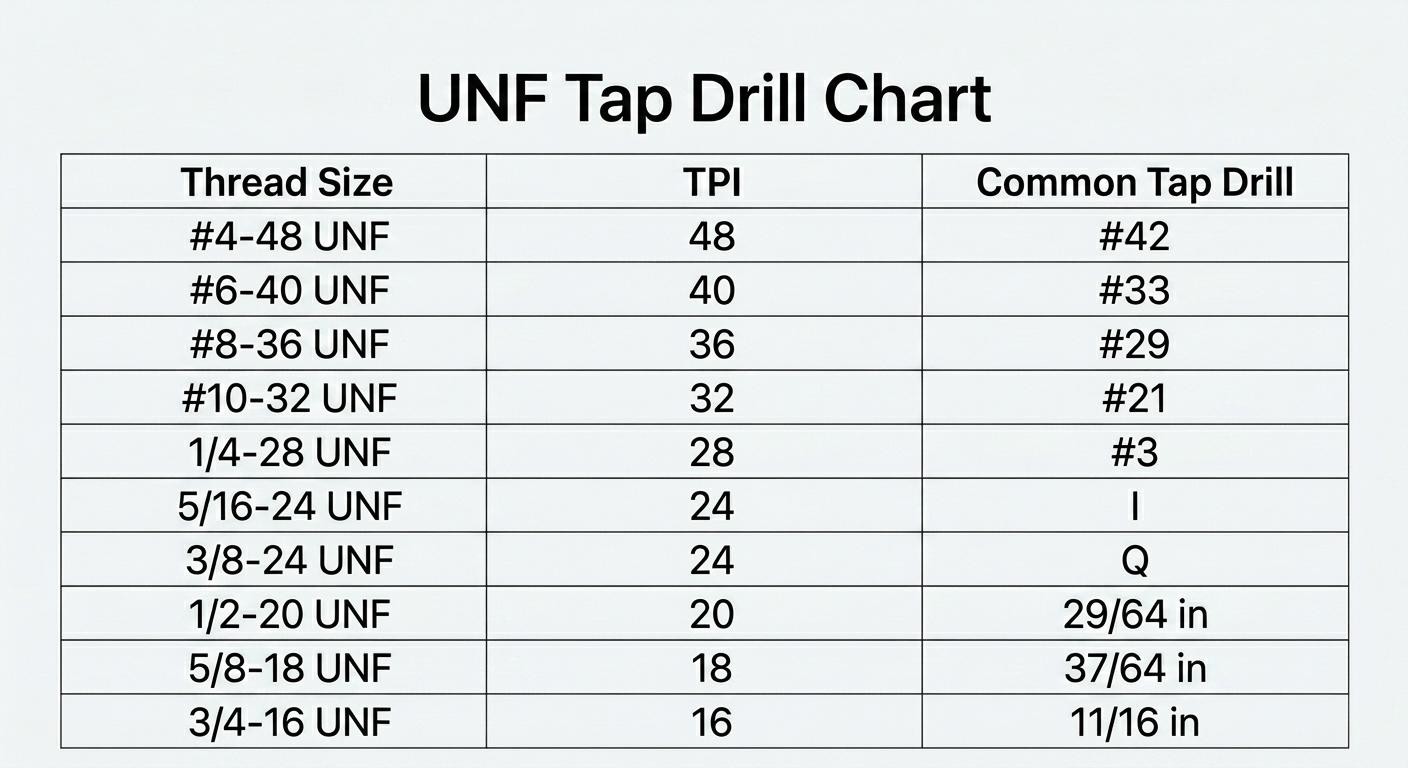
Chart values are common starting sizes for conventional cutting taps. The final drill size depends on the specified thread class, target percentage of full thread, workpiece material, tap geometry, and manufacturer's recommendations. Thread-forming taps require different hole-size data because they form the thread by displacing material rather than cutting it.
For further guidance on threaded-hole design, see our threaded hole guideline, which covers bottom-hole sizing, effective thread depth, thread inserts, and drawing requirements.
What Is a Drill and Tap Chart
A drill and tap chart is a reference used to match an internal thread size with the hole diameter required before tapping. It gives the machinist a starting hole size so the tap has enough material to form the thread without leaving the hole too small.
Engineers commonly check the chart when preparing:
- Technical Drawings
- Selecting Tooling
- Reviewing threaded features before production
The thread specification on the drawing determines which entry in the chart should be used. The chart is mainly a hole-size reference. It does not replace the thread callout on the drawing or the tooling manufacturer's recommendations for a particular material, tap type, thread class, and production application.
How to Read a Drill and Tap Chart
A drill and tap chart is easier to use when the thread callout is read in parts. The thread designation identifies the nominal size and pitch; the tap drill size gives the hole diameter to drill before tapping.
Metric Thread Size and Pitch
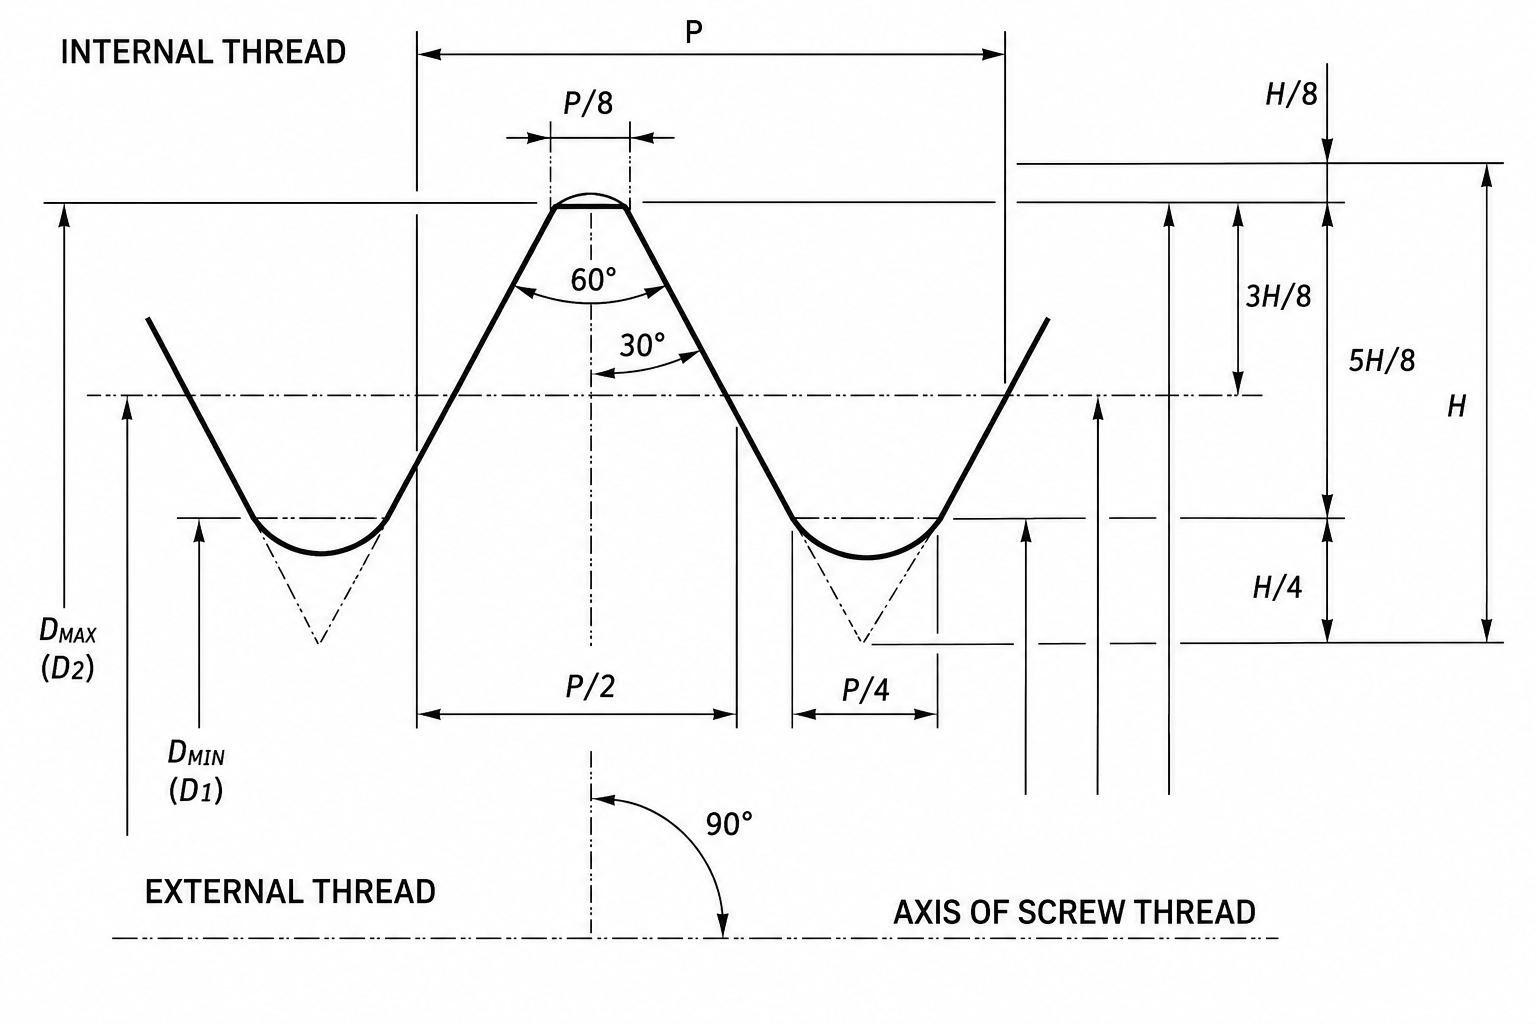
Metric threads are specified by nominal diameter and pitch in millimeters. For example, M6 x 1.0 indicates a 6 mm nominal diameter and a 1.0 mm pitch. Pitch is the axial distance between adjacent thread crests.
The same nominal diameter can use different pitches. M8 x 1.25 and M8 x 1.0 are both 8 mm threads, but they require different tap drill sizes. When reading a chart, the full designation should be matched rather than selecting a drill from the diameter alone.
ISO metric thread chart
UNC and UNF Thread Size and TPI
Inch threads are specified by nominal diameter and threads per inch (TPI). For example, 1/4-20 UNC has a 1/4-inch nominal diameter and 20 TPI, while 1/4-28 UNF has the same nominal diameter with 28 TPI.
The two threads therefore use different tap drill sizes. A chart entry cannot be selected from the nominal diameter alone; the thread series must also match the drawing. UNC is coarser, while UNF uses a finer pitch.
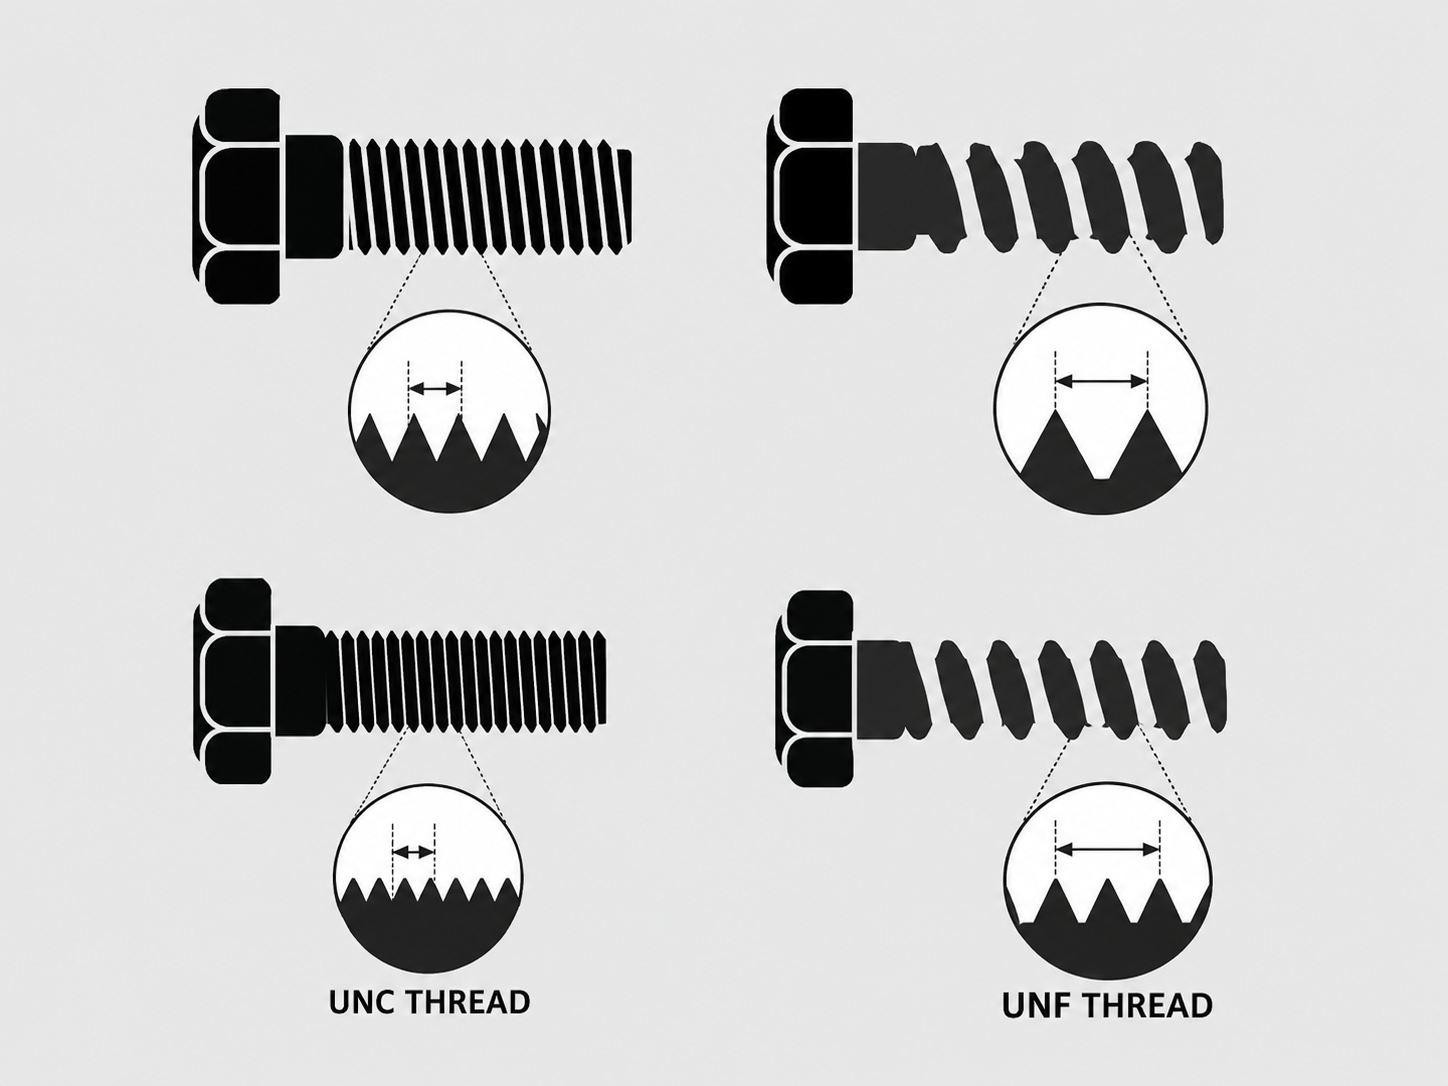
UNC and UNF thread profiles (Jarvis Cutting Tools)
Tap Drill Size and Thread Percentage
The tap drill size is the hole diameter prepared before the internal thread is cut. It is smaller than the nominal thread diameter because the remaining material forms the thread profile during tapping.
For example, a 1/4-20 UNC thread is not drilled with a 1/4-inch hole. The chart specifies a smaller pilot diameter so the tap has enough material to form the internal thread.
Tap drill charts may also list a percentage of full thread, which describes how much of the theoretical thread profile is produced by the tapped hole. This is different from effective thread engagement length, which refers to the axial length over which the internal and external threads engage. A larger tap drill generally produces a lower percentage of full thread, while a smaller tap drill produces a higher percentage. A longer tapped hole increases axial engagement, while changing the tap drill size changes the thread percentage.
On a production drawing, the chart value should be checked against the specified thread class and the tapping process. Material hardness, tap geometry, coating, and machine setup can affect the practical hole size, particularly in harder alloys or when cutting deep blind holes.
CNC Drilling and Tapping Process
A CNC machine normally makes a tapped hole in two main cutting stages: drilling the starting hole and cutting the internal thread. The finished hole is then checked against the drawing requirement before the part moves to the next operation.
Drilling Before Tapping
The hole is drilled first to the required starting diameter and depth. For a blind hole, the drilled depth needs to allow enough room below the specified thread length because the drill point and the end of the tap do not produce a fully threaded area at the very bottom.
The hole should also be clean and free of chips before tapping. On a CNC machine, the drilling operation is programmed with the required position, diameter, and depth from the part drawing.
CNC Tapping Process
During rigid tapping, spindle rotation and axial feed are synchronized with the thread pitch, allowing the tap to advance one thread pitch per revolution. The tapping cycle must match the specified thread size, pitch, hole depth, material, and tap type.
Blind holes require particular attention to the programmed depth because the tap needs clearance below the required effective thread length.
Additional clearance below the required effective thread depth may be necessary in blind holes, depending on the drill point, tap geometry, and required thread depth. Deep or unusually long tapped holes may require specialized tooling and additional machining time.
Thread Inspection
After tapping, the thread is checked to confirm that it matches the drawing. Internal threads are commonly verified with GO and NO-GO plug gauges selected for the specified thread class and tolerance.
Inspection should verify more than the presence of visible threads. Depending on the drawing, the check may include thread size, gauge acceptance, effective thread depth, hole position, and damage to the threaded surface.
For CNC parts with internal threads, include the thread designation, effective thread depth, and hole type on the drawing. JLCCNC can review threaded features during quoting and DFM.
Precision CNC Machining Service
Professional manufacturing, fast turnaround, and quality assurance.
Factors Affecting Tap Drill Size Selection
The tap drill is selected from the thread requirement, but the final hole size also depends on how the hole will be used and machined. Material, hole depth, and the amount of thread engagement are the main points to check before putting the hole on a CNC drawing.
Material Considerations
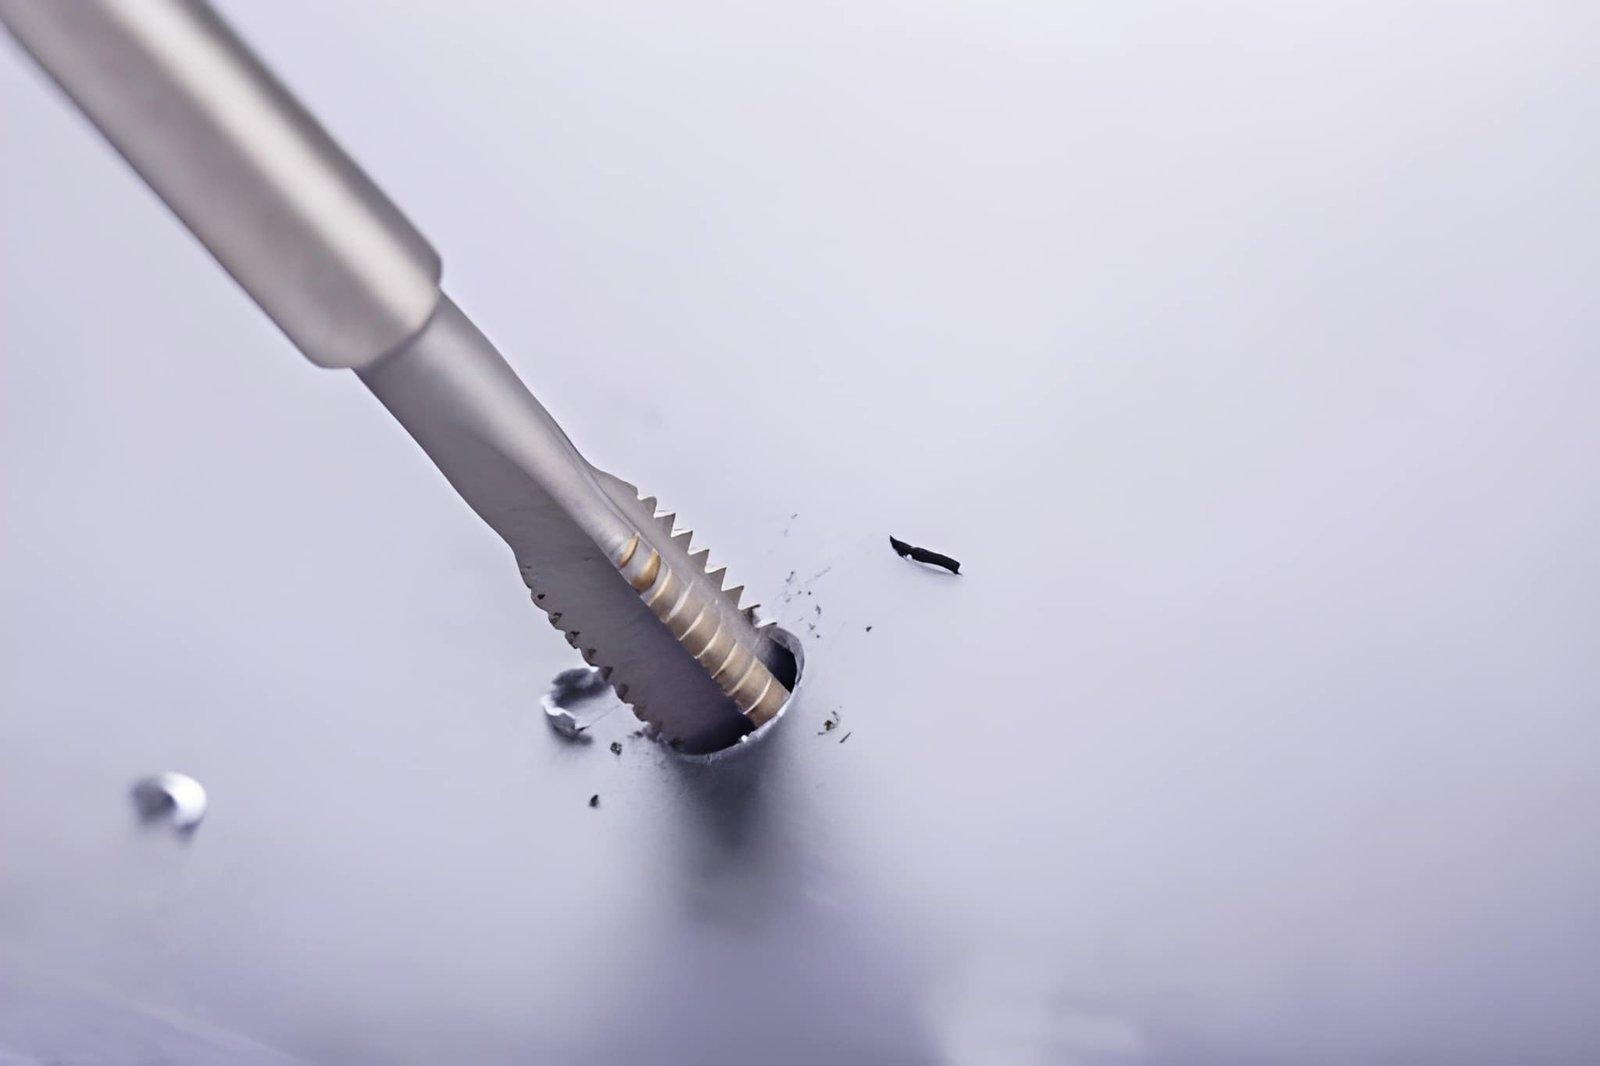
Tap drill for aluminum alloy CNC machining (iStock)
The workpiece material affects the cutting load on the tap. Material affects cutting torque, chip formation, and tap life. Aluminum and many brass alloys generally require less tapping torque than stainless steels and other difficult-to-machine materials, but the exact drill size should still follow the tap manufacturer's recommendation.
This matters when a drawing specifies a threaded hole in a difficult-to-machine material. The tap supplier's recommended drill range should be checked rather than assuming that the same hole size is suitable for every material.
Blind Holes vs Through Holes
Blind tapped hole showing effective thread depth and bottom clearance (ScienceDirect)
A through hole gives the tap space to pass completely through the part. For a blind tapped hole, the drilled depth must exceed the required effective thread depth to provide clearance for the drill point and the tap chamfer or runout.
For example, if a blind hole requires 10 mm of effective M5 thread depth, the 10 mm dimension should not be used as the total drilled depth. Additional depth is required below the effective thread to accommodate the drill point and the tap's incomplete-thread region. Space is needed below the usable thread because the drill has a point, and the tap cannot produce a full thread at the bottom of the hole.
For a blind hole, the total drilled depth should provide the required effective thread depth plus sufficient clearance for the drill point and the unthreaded portion created by the tap chamfer.
Thread Engagement Requirements
Do not specify a deep thread simply because more thread engagement sounds stronger. Once sufficient engagement is available for the joint, additional thread length can add machining time without providing a useful benefit.
As a JLCCNC DFM guideline, effective thread depth is generally kept to about three times the hole diameter under standard machining conditions. This is a manufacturability guideline rather than a universal strength requirement. Deeper threads may be possible, but they can require special tooling and increase machining time and cost.
For the drawing, specify the effective thread depth rather than assuming that the total drilled depth is the same as the usable thread depth.
Common Drill and Tap Issues
When thread quality is poor, inspect the finished hole, tap condition, chip evacuation, and tapping cycle to identify the actual cause before changing the process.
Poor Thread Quality
Poor thread quality can appear as rough or damaged thread flanks, incomplete thread forms, or failure of the specified GO/NO-GO gauge inspection.
Check the finished hole with the specified thread gauge. If the thread is damaged, inspect the tap for wear or chipped cutting edges and check whether chips were left in the hole during machining.
The correction depends on the cause. A worn tap should be replaced, while chip buildup requires cleaning the hole and improving chip removal during the operation.
Tap Breakage
Broken CNC tap in a blind threaded hole (Yamawa)
A broken tap leaves part of the tool inside the threaded hole and can make the part difficult to recover. Before attempting removal, check where the tap broke and the condition of the hole.
Inspect the tap for damage and check for chip buildup, excessive tool wear, tapping-cycle problems, or contact with the bottom of a blind hole. If the same tap keeps breaking during production, the machining setup should be checked rather than simply replacing the tool each time.
Drill and Tap Chart FAQs
How Do I Find the Correct Tap Drill Size?
Here is the simple approach:
- Check the thread size and pitch on the drawing first.
- Then find that exact thread in the tap drill chart and use the listed drill size as the starting hole.
- For production work, check the tap manufacturer's recommended size as well, since the required hole can change with the tap type and material.
What Drill Size Is Used for M6 Tapping?
For a standard M6 x 1.0 thread, use a 5.0 mm drill as the common starting size for a cutting tap. M6 with a different pitch will need a different drill size.
What Drill Size Is Used for 1/4-20 Tapping?
A #7 drill is the common starting size for a 1/4-20 UNC cutting tap. The hole size can be adjusted when a particular thread fit or tap manufacturer's specification requires it.
Is Tap Drill Size the Same as Thread Size?
The two sizes are different. The tap drill is smaller because the tap needs material left around the hole to cut the internal thread. For example, an M6 x 1.0 thread normally starts with a 5.0 mm hole, not a 6 mm hole.
Can CNC Machines Create Tapped Holes?
A CNC machining center can drill and tap holes in the same setup. The machine first makes the starting hole, then uses a tapping cycle to cut the internal thread. The finished hole can be checked with a suitable thread gauge before the part is released for assembly.
What is a tap drill?
A tap drill is the drill used to create the hole before an internal thread is cut with a tap. Its diameter is smaller than the nominal thread diameter and is selected to provide the required thread percentage and tapping clearance.
Precision CNC Machining Service
Professional manufacturing, fast turnaround, and quality assurance.
Conclusion About Drill and Tap Charts
A tap drill chart tells you which hole size to prepare before tapping a thread. Start with the exact thread designation on the drawing, then match it to the corresponding drill size. A small change in pitch or TPI can change the required hole diameter.
For CNC machining, the drill size should also match the tapping method. A cutting tap removes material as it forms the thread, while a forming tap displaces it. The recommended hole size can therefore differ, especially when the drawing calls for a specific thread fit.
For CNC parts with tapped holes, upload the CAD model and 2D drawing to JLCCNC for review and quotation. Thread specifications can be checked against the machining process before production.
Popular Articles
• Cutting with Precision: A Comprehensive Guide to CNC Water Jet Technology
• CNC Coolant Explained: Types, Maintenance & Safety
• Rake Angle in Machining: Machinists’ Guide to Perfect Cuts
• What Steps Are Taken To Minimize Waste In CNC Machining Processes?
• How EDM Wire Cutting Works: Complete Guide to Precision CNC Wire Cutting
Keep Learning
Flange Machining: CNC Process and Custom Manufacturing Guide
Key Takeaways Flange machining can create faces, bores, grooves, holes, threads, hubs, and steps. Material affects machinability, corrosion resistance, weight, and mechanical performance. Datum relationships and flange geometry can influence sealing, alignment, and assembly. Custom production supports non-standard interfaces, prototypes, and low-volume orders. Inspection verifies dimensions, geometry, surface condition, and drawing requirements. An RFQ should include design files, mating information, ......
Sheet Metal vs CNC Machining: A Guide to Choosing the Right Method for Your Metal Parts
When it comes to fabricating metal parts, people often face the dilemma of choosing between sheet metal fabrication and CNC machining. Each method offers unique advantages, and the decision depends on various factors such as part complexity, precision requirements, cost considerations, and production volume. In this article, we will delve into the characteristics of sheet metal fabrication and CNC machining, helping you make an informed decision on the optimal method for your specific metalworking nee......
CNC Workholding: How to Choose Fixtures & Locating Methods
CNC workholding refers to the methods used to position and secure a part during machining. It directly affects part dimensions, alignment, and surface finish. In practice, machining errors are rarely caused by the toolpath alone. More often, they originate from poor part positioning, uneven clamping, or material deformation under cutting forces. For operations requiring tight tolerances, like ±0.01 mm, a stable and properly designed workholding setup is just as important as the machine’s spindle accur......
Blade Machining: CNC Milling & 5-Axis Guide
Key Takeaways Blade machining follows a changing airfoil shape, so the profile, twist, thickness, and edge geometry have to stay within the drawing requirements. 5-axis CNC milling gives better access to twisted and curved blade surfaces and can reduce the need to reposition the part. Cutter position and tool orientation have a direct effect on surface finish, cutting load, and access around the airfoil. Thin blade sections need proper support during machining because cutting forces can change the fin......
CNC Meaning: Definition and What It Stands For
What Is CNC? Realistic factory photo of a CNC milling machine cutting aluminum with coolant spray, technician in the background. CNC Definition and Acronym Explained CNC, short for Computer Numerical Control, refers to a manufacturing method in which machine tools are controlled by pre-programmed computer instructions rather than manual operation. These instructions define tool movement, speed, feed rate, and machining sequence, allowing machines to perform cutting, drilling, milling, and shaping task......
Threaded Inserts for Plastics: A Complete Guide to Types and Applications
Key Takeaways Threaded inserts provide reusable metal threads in plastic parts and can improve retention and assembly repeatability compared with directly tapped plastic threads. Common insert types include press-in, self-tapping, heat-set, ultrasonic, and molded-in designs, with each suited to different materials and production conditions. Heat-set inserts are widely used for thermoplastic and FDM applications, while press-in and self-tapping inserts offer alternatives when heat installation is unsui......